Dirty water pumps
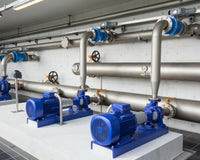
Dirty water pumps are used to transport liquids containing solid particles (sand, silt, fibers, small stones) or chemical admixtures. In practice, this includes both emergency pumping of a flooded basement and continuous pumping of wastewater in a household or transfer of process media in industrial plants. Key challenges include resistance to abrasion, the risk of clogging, and maintaining capacity as pressure losses increase. A properly selected pump reduces service costs and installation downtime. Matching the model correctly to the medium also reduces electricity consumption.
In market terminology, the terms dirty water pumps and contaminated water pumps are used interchangeably. Selection always begins by defining the medium: solid fractions (in mm), viscosity, density, temperature, and the potential presence of fibers and elements that could block the impeller. Analyzing these parameters makes it possible to predict local and linear losses in the piping. This makes it easier to determine the duty point and expected pump capacity.
Basic tasks include: removing dirty water from flooded rooms, pumping dirty water to the sewage system or a tank, as well as pumping contaminated water over longer distances with the help of check and shut-off valves. In each case, the Hmax parameter, passage size, and impeller geometry have different significance. Therefore, before purchasing, it is worth carrying out at least simplified hydraulic calculations.
Types of dirty water pumps
Three main equipment families are most commonly encountered: submersible pumps, diaphragm pumps, and impeller pumps. Selection depends on the required pump capacity, required head, and type of contaminants. In many installations, a mixed configuration is also suitable—for example, pumps for water and septic tanks in one facility (house + household wastewater treatment plant), where different media are handled by different sections of the system. The choice should also take operating frequency and service requirements into account. The availability of spare parts and local service can also be important.
- Submersible pumps: compact, equipped with a float switch, and designed for operation in a tank or sump. Excellent for emergency water removal and intervention work. They are characterized by simple installation and mobility in the field. Versions with a cooling jacket are better suited to prolonged operating cycles.
- Diaphragm pumps: highly resistant to fibrous contaminants and dense media, with a lower risk of damage from solids, but usually offering lower pumping capacity than impeller models. They perform well with liquids of increased viscosity. Their advantages include simple and quick servicing.
- Impeller pumps: a wide range of power ratings and impeller geometries (channel, Vortex, grinder). They dominate in domestic and industrial installations, including pressurized sewer systems. They allow the operating point to be precisely matched to the required capacity. With the right fittings, they achieve high system efficiency.
Submersible pump for dirty water
A submersible pump for dirty water is the most popular solution in single-family housing. The unit operates in the medium, the motor is cooled by the flow, and float automation protects against dry running. Typical applications include pumping out water after flooding, lowering the groundwater level in an excavation, and pumping dirty water from a collection well into the sewer system. Its advantages include low weight and easy transport to the site of a failure. With the correct passage diameter, you can minimize the risk of blockages.
Key specification elements include: maximum head, minimum suction level, solids passage diameter, type of seals, and equipment power. Remember that the catalog Hmax is not the operating point—the actual intersection with the system curve (linear and local losses) is usually lower. Therefore, when planning dirty water pumping through a long discharge hose, select a unit with a reserve capacity. Simulating pressure drops in the hose will help avoid undersizing in advance. For permanent installations, measuring the actual medium inflow is recommended.
Submersible pumps for dirty water
Submersible pumps for dirty water offer a wide range of outlet diameters and impeller geometries: from open impellers, through channel impellers, to Vortex and grinder impellers. Models with Vortex impellers have greater tolerance for solids, but their efficiency may be lower—this is worth factoring in if economical dirty water pumping is important. When selecting a pump, also consider the nature of the liquid inflow and cycle frequency. In environments containing fibers, pre-shredding provides better results.
For cyclic operation, the durability of mechanical seals is crucial (often in an oil bath). In applications involving fibers (cloths, wipes) found in domestic wastewater, consider a macerator module or dedicated septic tank pumps with a macerator. This reduces the risk of downtime caused by the need for cleaning. An additional safeguard may be a basket pre-filter.
Diaphragm pumps
Diaphragm pumps perform well when the medium is denser and the flow contains particles with varied structures (fibers, suspended solids). Although their pump capacity may be lower, they are valued for their resistance to dry running and simple operation. On farms, they are used to transfer dense liquids, while in construction they serve auxiliary tasks where reliability is important. Their design facilitates quick servicing and replacement of wear parts. They also handle abrasive media well at moderate pressures.
Impeller pumps
Impeller pumps (with open, channel, Vortex, or cutting impellers) offer the widest range of parameters, from small mobile units to stationary pump sets. In domestic and municipal installations, they are standard for pumping contaminated water and in pressure sewer systems. Selecting the right impeller directly translates into a lower risk of clogging and stable pumping capacity. In industrial applications, they enable precise control of flow and pressure. Their efficiency can be further improved by optimizing the valve system and pipe diameters.
Applications of dirty water pumps
The range of applications is very broad: from dewatering and drying floors, through operation in household tanks and garden ponds, to industrial systems with solids separators. In agriculture, slurry pumps have a special role, while in urban infrastructure, pressure sewer pumps are particularly important. In all cases, the primary objective is the reliable removal of dirty water and safe transfer of the medium to the receiving point. Appropriate automation reduces the risk of dry running and motor overheating. Regular servicing extends the service life of the entire system.
Dewatering pumps
Dewatering pumps are designed to operate in demanding environments involving fine gravel, silt, sand, and frequent relocation. Important features include a robust housing, a stabilizing base, and easy access to the suction strainer. If the discharge line is long, pay attention to the diameter selection—a diameter that is too small dramatically increases losses and reduces pump capacity. A good practice is to use long-radius bends and fittings with an enlarged flow passage. Versions with increased abrasion resistance handle the transport of mineral suspensions better. Portable handles make it easier to respond quickly to changing conditions on the construction site.
Pressure sewer pumps
Pressure sewer pumps work with hermetic tanks and pump wastewater to the collector sewer. They often use grinder impellers to minimize the risk of blockages in sections with small diameters. In this case, the maximum head and operating characteristics under variable loads are important. If fibers are present in the flow, a unit with a cutting knife and appropriately selected thermal protection is a good choice. For stable operation, it is worth providing a check valve with a large flow passage. A level monitoring system reduces the risk of backflow during network failures.
Slurry pumps
Slurry pumps must handle a medium with increased viscosity and organic suspended solids. The preferred options are wear-resistant designs and submersible pumps with agitators that homogenize the tank contents. Due to the demanding operating conditions, regular inspection of the seals and impeller condition, along with convenient service access, is essential. Properly selected impeller geometry reduces the risk of clogging with fibers. Extra power during startup makes it easier to move the dense medium.
Septic tank pumps with a grinder
Septic tank pumps with a grinder solve the problem of fibrous contaminants and elements that could block the flow. The cutting assembly shreds waste before it reaches the impeller, enabling stable pumping of dirty water through a thin PE pipe, even over longer distances. This is the basic choice when the wastewater drainage system has limited diameters or an unusual layout. It is worth ensuring easy disassembly and access to the cutting components. Regular blade inspections maintain flow performance.
Water pumps and septic tank pumps
Water and sewage pumps is a colloquial term for systems that handle different media at one site: rainwater, contaminated water, and wastewater. It is important to ensure proper separation of circuits and separate fittings—the requirements for pumping contaminated water differ from those for roof runoff. Reliability and ease of servicing remain the common denominators. A good practice is to use separate check valves for each line. Periodic inspections will reduce the risk of odors migrating and backflow.
Rainwater pumps
Rainwater pumps are used to supply garden irrigation, surface cleaning, and maintenance work. Although the water is relatively clean, small contaminants such as leaves and dust occur in tanks, so pre-filtration is necessary. In infiltration and retention systems, stable flow parameters and energy efficiency are required. Systems with pressure automation and a diaphragm tank work well. Selecting the appropriate power reduces operating costs.
Clean water pumps
Clean water pumps complement the range—they are found in pressure-boosting systems, pressure tanks, and irrigation sets. In this article, we discuss them as a supporting topic to highlight the design and operational differences compared with units for dirty water. They most often use higher-efficiency impellers with smaller passageways. They also require cleaner fittings and more thorough pre-filtration.
Submersible pumps
Submersible pumps are characterized by simple installation and mobility. Versions with a cooling jacket are better suited to continuous operation in sumps with limited flow. When selecting a model, pay attention to the minimum suction level and access to the suction basket—it retains larger particles, protecting the impeller and seals. An appropriately long power cable improves work safety. In difficult conditions, plugs and connectors with enhanced watertightness are recommended.
Floor drying pumps
Floor drying pumps feature a low-suction design and make it possible to collect a thin layer of water (so-called “mop-dry” level). They are useful after flooding, in industrial halls, and in underground garages. It is worth choosing models with quick couplings and a lightweight hose so the team can respond quickly and efficiently carry out dirty water removal after rainfall. The low overall weight makes maneuvering in tight spaces easier. The base’s high mechanical resistance reduces the risk of damage during frequent relocation.
Selection parameters: from flow rate to head
Effective selection is based on five pillars:
- Pump capacity – the minimum required flow rate (m3/h or l/min) resulting from the tank emptying time or the rate of water inflow.
- Maximum head – Hmax should have a margin above the installation requirements; remember linear losses (length, diameter, roughness) and local losses (elbows, valves).
- Pumping capacity at the duty point – check the manufacturer’s curve; do not rely on extreme values.
- Device power – underestimating it leads to overheating and reduced service life, while overestimating it leads to unnecessary energy costs.
- Water lift parameters – account for the geometric height, level differences, and the water level height in the well.
In practice: if you plan to pump dirty water several dozen meters through a thin PE pipe, account for greater losses – consider a larger diameter or a grinder to maintain a stable flow. It is also worth installing a check valve to reduce water hammer. Additional air-venting points will facilitate commissioning and servicing.
Dirty water pumps
The term dirty water pumps covers a full range of designs and power ratings – from portable emergency models to stationary units. In single-family homes, compact devices with a float are most commonly used; in construction, versions with increased resistance to abrasion; and in infrastructure, grinder units designed for operation in pressurized networks. An informed selection shortens installation and commissioning time. Extra capacity reduces the risk of unplanned downtime.
Dirty water pumps – what to watch out for during operation
When working with a “dirty water” medium, inlet filtration and control of start/stop cycles are crucial. Frequent short cycles overheat the motor, which is why float automation and the correct capacity of the equalization tank are so important. Maintenance includes inspecting the suction strainer, checking the tightness of the lines, verifying the condition of the impeller, and inspecting the check valves. It is also worth monitoring the starting current and housing temperature. In abrasive environments, anti-sand guards can be helpful.
Sewage pump – selection and installation
A typical septic tank pump should have a large solids passage or a grinder. Important factors include chemical resistance, impeller design, thermal protection, and service access. Installation is planned in a sump with easy removal on guide rails; a check valve and shut-off valve are mandatory on the discharge side. It is worth providing an emergency power supply or a bypass system in case of a power outage. An overflow sensor and audible alarm will improve operational safety. Some solutions also allow installation on a coupling foot, so it is worth checking the available installation options before choosing a pump and asking the seller about the solution best suited to your needs.
Pumps for pond water
Pumps for pond water must combine gentle operation with resistance to biological contamination. Impellers with increased free passage and pre-filtration are recommended. In cascade systems, a stable Hmax is important to maintain the visual effect and the proper flow through the filter. Regular maintenance limits the growth of algae and sediment. It is worth adding a UV filter when water clarity is important.
Which submersible pump should you choose?
If you are wondering which submersible pump to choose for your application, start with these questions: What is the discharge route? What are the pipe diameters? What medium are we working with (particles and fibers)? What tank emptying time is required? Where is the receiver located? What is the water level height? With this information, you can select the appropriate impeller geometry and a reserve of maximum lifting height. Also consider the power supply and electrical protection conditions. For seasonal operation, quick disassembly and compact dimensions are useful.
Types of drainage pumps
Types of drainage pumps differ in power range, suitability for mobile operation, and resistance to abrasion. Construction versions have reinforced bases, protected power cables, and convenient carrying handles. For continuous operation, it is worth considering level sensors and overflow alarms. Additional inlet grilles limit the intake of large particles. It is worth allowing space for quickly rinsing the suction basket.
Types of submersible pumps
Types of submersible pumps include both compact units for emergency work and stationary systems with guide rails. The choice of impeller (open, channel, Vortex, or with a grinder) determines tolerance to solids and susceptibility to clogging. It is worth considering the quality of the seals and the type of bearings. Selecting appropriate housing materials increases durability in aggressive environments.
Suction and lifting – what they affect
In submersible pumps, the water suction stage is shorter because the impeller operates directly in the medium. However, the final result is determined by system losses and the water head. The longer and narrower the discharge line, the greater the drop in flow rate—therefore, for projects with long sections, we recommend calculating the losses before purchase. Optimizing the diameters and number of elbows can significantly improve the operating point. Air vents should also be provided at the highest sections of the system.
Selection and operation checklist
- Define the medium: “contaminated dirty water” containing fibers? sand? grease?
- Match the impeller and free passage: Vortex / channel / grinder.
- Determine the pumping capacity and the Hmax margin.
- Select discharge diameters and fittings (a check valve with an enlarged passage).
- Ensure service access and pre-filtration.
- Configure the automation (float switch, thermal protection, signaling).
- Schedule seasonal inspections and clean the suction basket.
Need help choosing? Visit Dambat – a manufacturer and distributor of pumping solutions in Poland. Consulting an advisor shortens the selection process and reduces the risk of mistakes. Preliminary site data makes it possible to precisely match the pump capacity to the conditions.
Frequently asked questions (FAQ)
Dirty water pump – what is it?
It is a device for transporting liquids containing solid contaminants. Depending on the application, submersible pumps, diaphragm pumps, or impeller pumps are used. The key is selecting the impeller and free passage according to the size of the solids. The right geometry reduces the risk of blockages and drops in performance. Regular servicing ensures long-lasting, stable operation.
What is the difference between a dirty water pump and a septic tank pump?
Dirty water pumps are designed for liquids containing mineral solids (sand, silt, small stones) and usually use channel or Vortex impellers with a larger free passage, but without a cutting assembly. They perform better where contaminants are short and non-stringy and discharge lines are of moderate length.
Septic tank pumps handle domestic wastewater containing fibers and long objects, so they often feature a grinder, reinforced seals, and suitability for aggressive environments. In pressurized sewage systems and when pumping through thin PE pipes, they minimize the risk of blockages and backflow by shredding contaminants before they reach the impeller.
How do you choose the discharge hose diameter for a submersible pump?
The diameter should match the manufacturer's recommended passage size to avoid restricting the flow and increasing friction losses. A cross-section that is too small will reduce pumping performance and may cause the motor to overheat. For long sections, consider using a larger diameter than the minimum. Confirm the final selection by calculating the losses and checking the operating point.
Can a dirty-water pump run dry?
No, most models are not designed for this, and dry running leads to seal damage and overheating. Selected diaphragm pumps are an exception, but they also have time limitations. Always use a float control system or a dry-run sensor. Also monitor the minimum liquid level required for cooling.
Which impeller should you choose: Vortex, channel, or grinder?
A Vortex impeller has a high tolerance for solids but usually lower efficiency. A channel impeller provides better efficiency when the particles are small and uniform. A grinder impeller is suitable for fibers and long items typical of domestic wastewater. Make your choice based on the medium's composition and the required Hmax.
How can you prevent a sewage pump from clogging?
Use sewage pumps with grinders and regularly inspect the inlet basket and the condition of the blades. Avoid disposing of non-degradable materials and long fibers. Plan for easy removal of the pump on guide rails for quick inspection. Remember to use a check valve with an enlarged passage.
What does the maximum head (Hmax) in practice?
This is the maximum height of the water column at which the flow drops to zero, so it is not a realistic operating point. In practice, the pump operates effectively at lower values, where the pump curve intersects the system curve. Therefore, always leave some headroom Hmax relative to the calculated demand. The impact of local losses and pipe diameter can be significant in long lines.
Where to buy IBO equipment?
You can buy our IBO products on the B2B platform. If you are an end customer, we encourage you to check our partner stores and wholesalers. You can also always contact us: +48 22 721 11 92, biuro@dambat.pl.