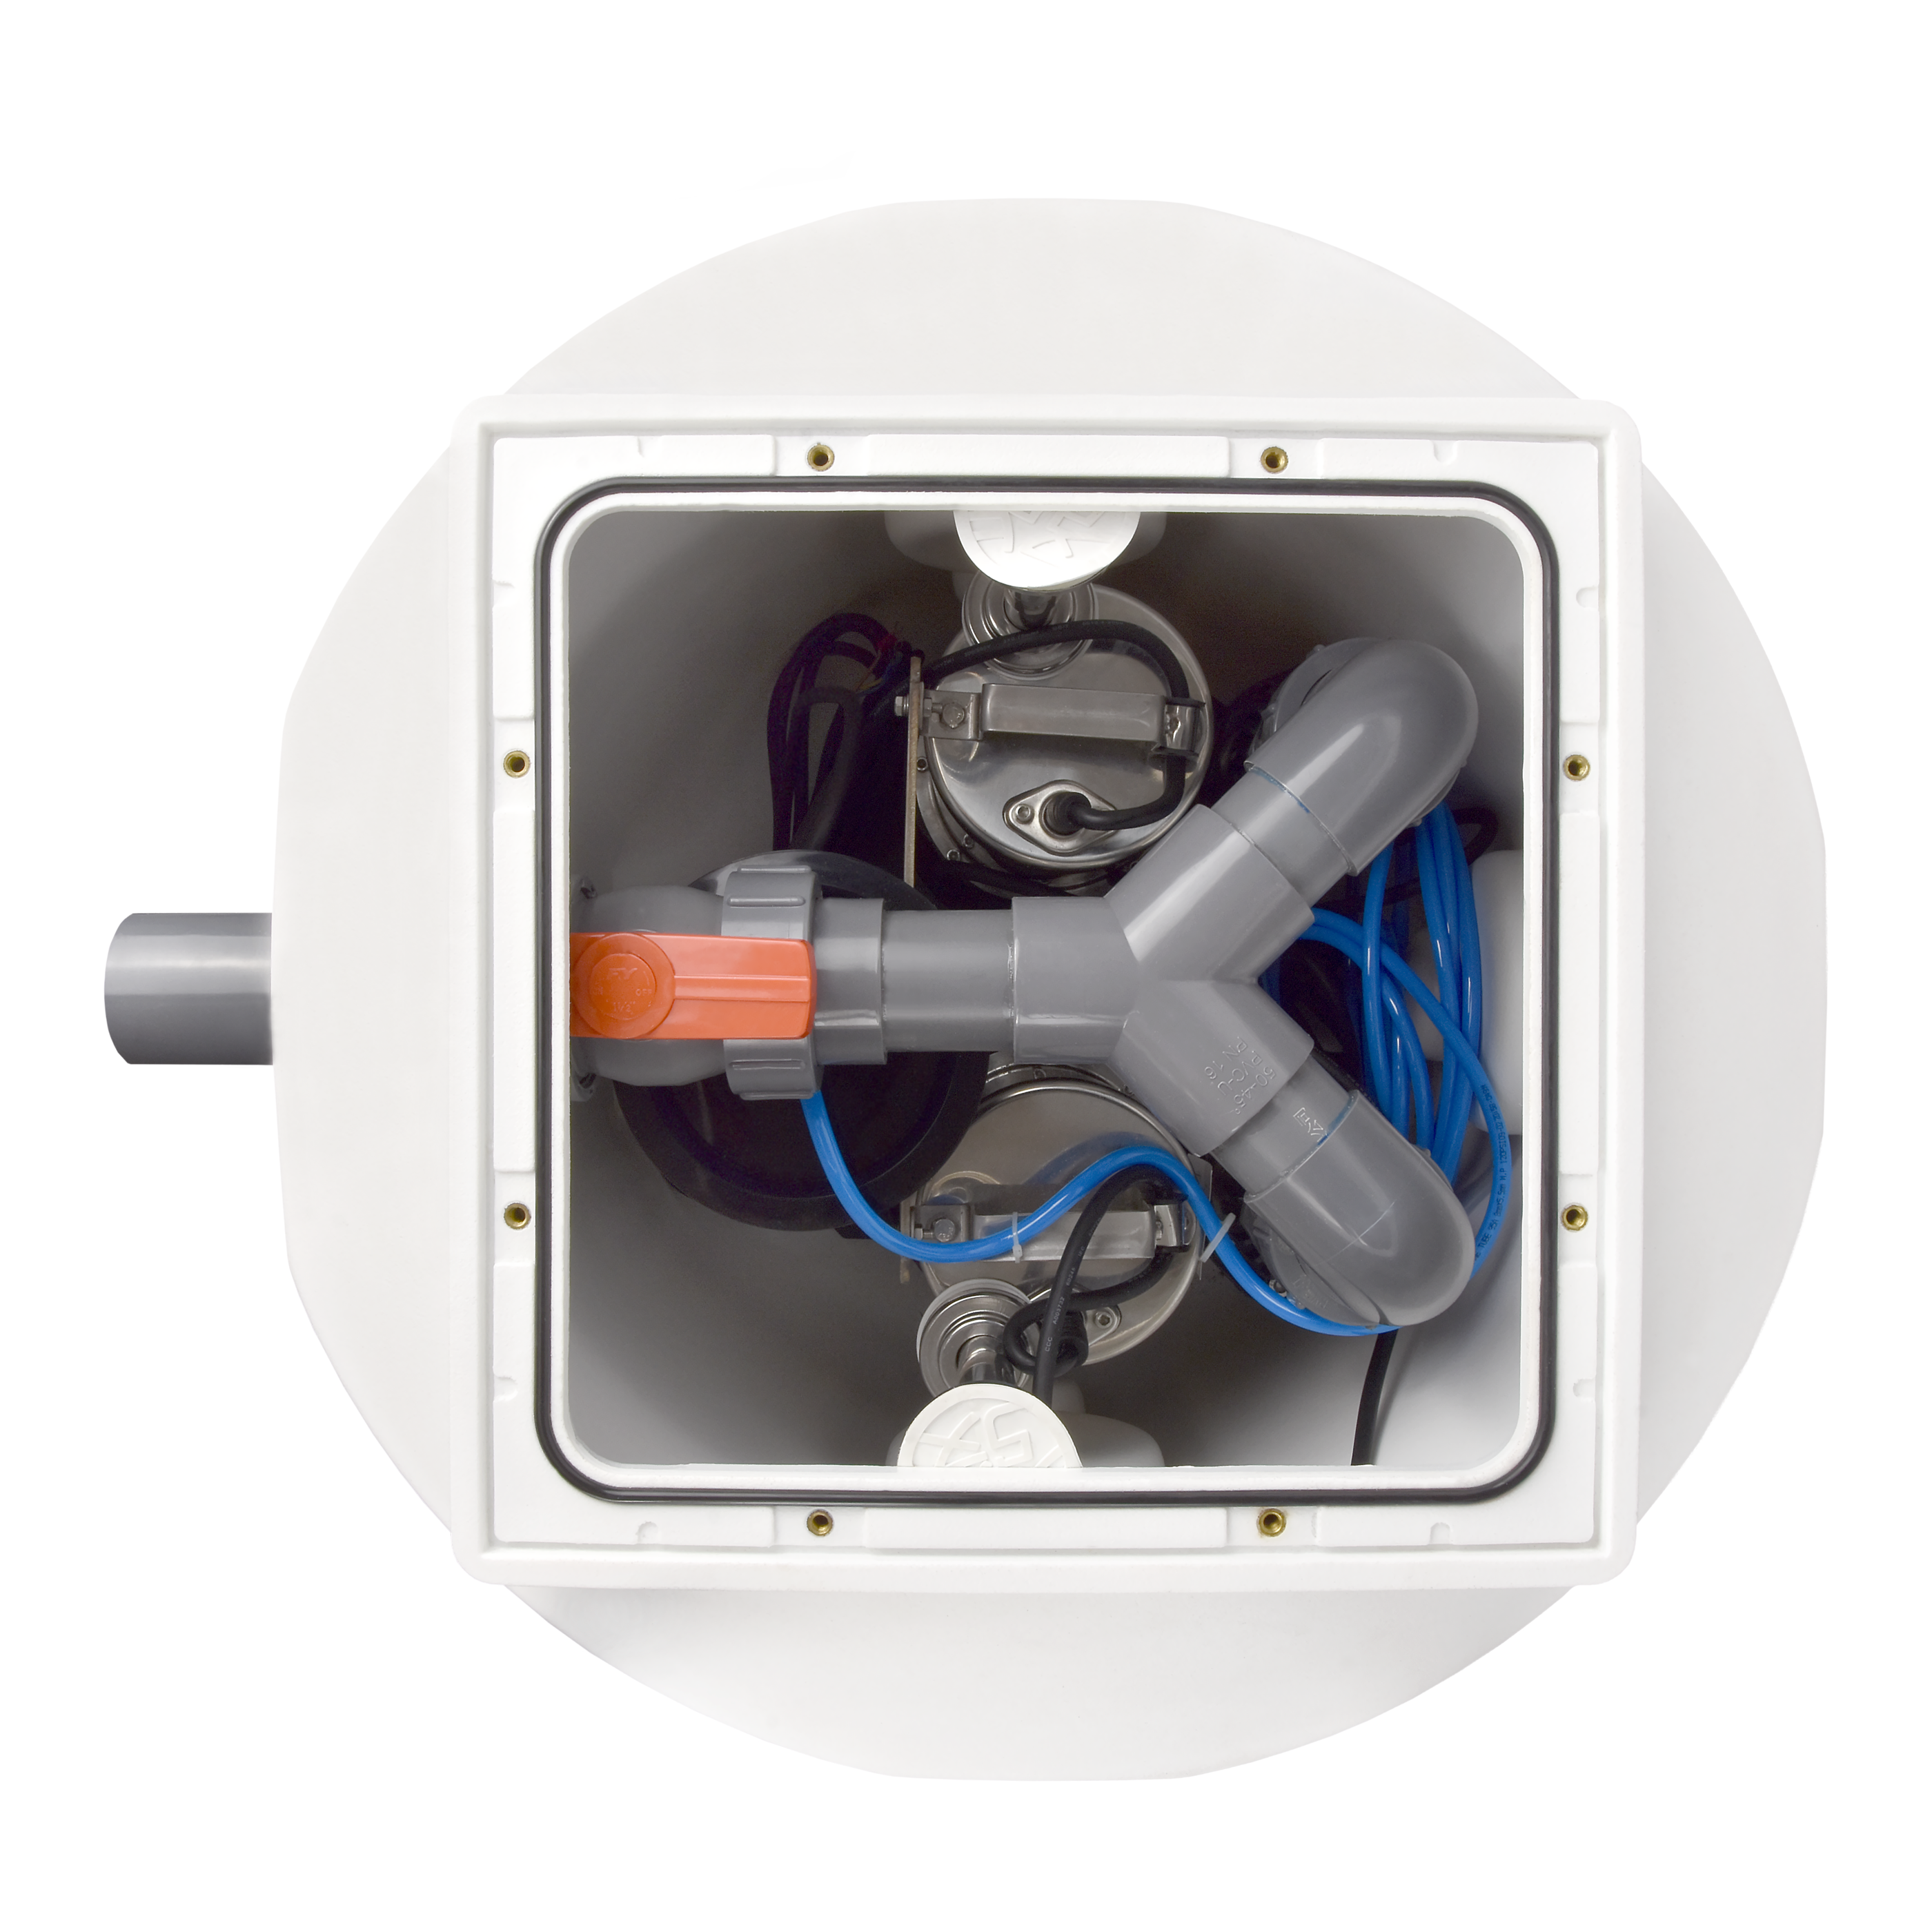
SANBOX HB – IBO lifting station
Application:
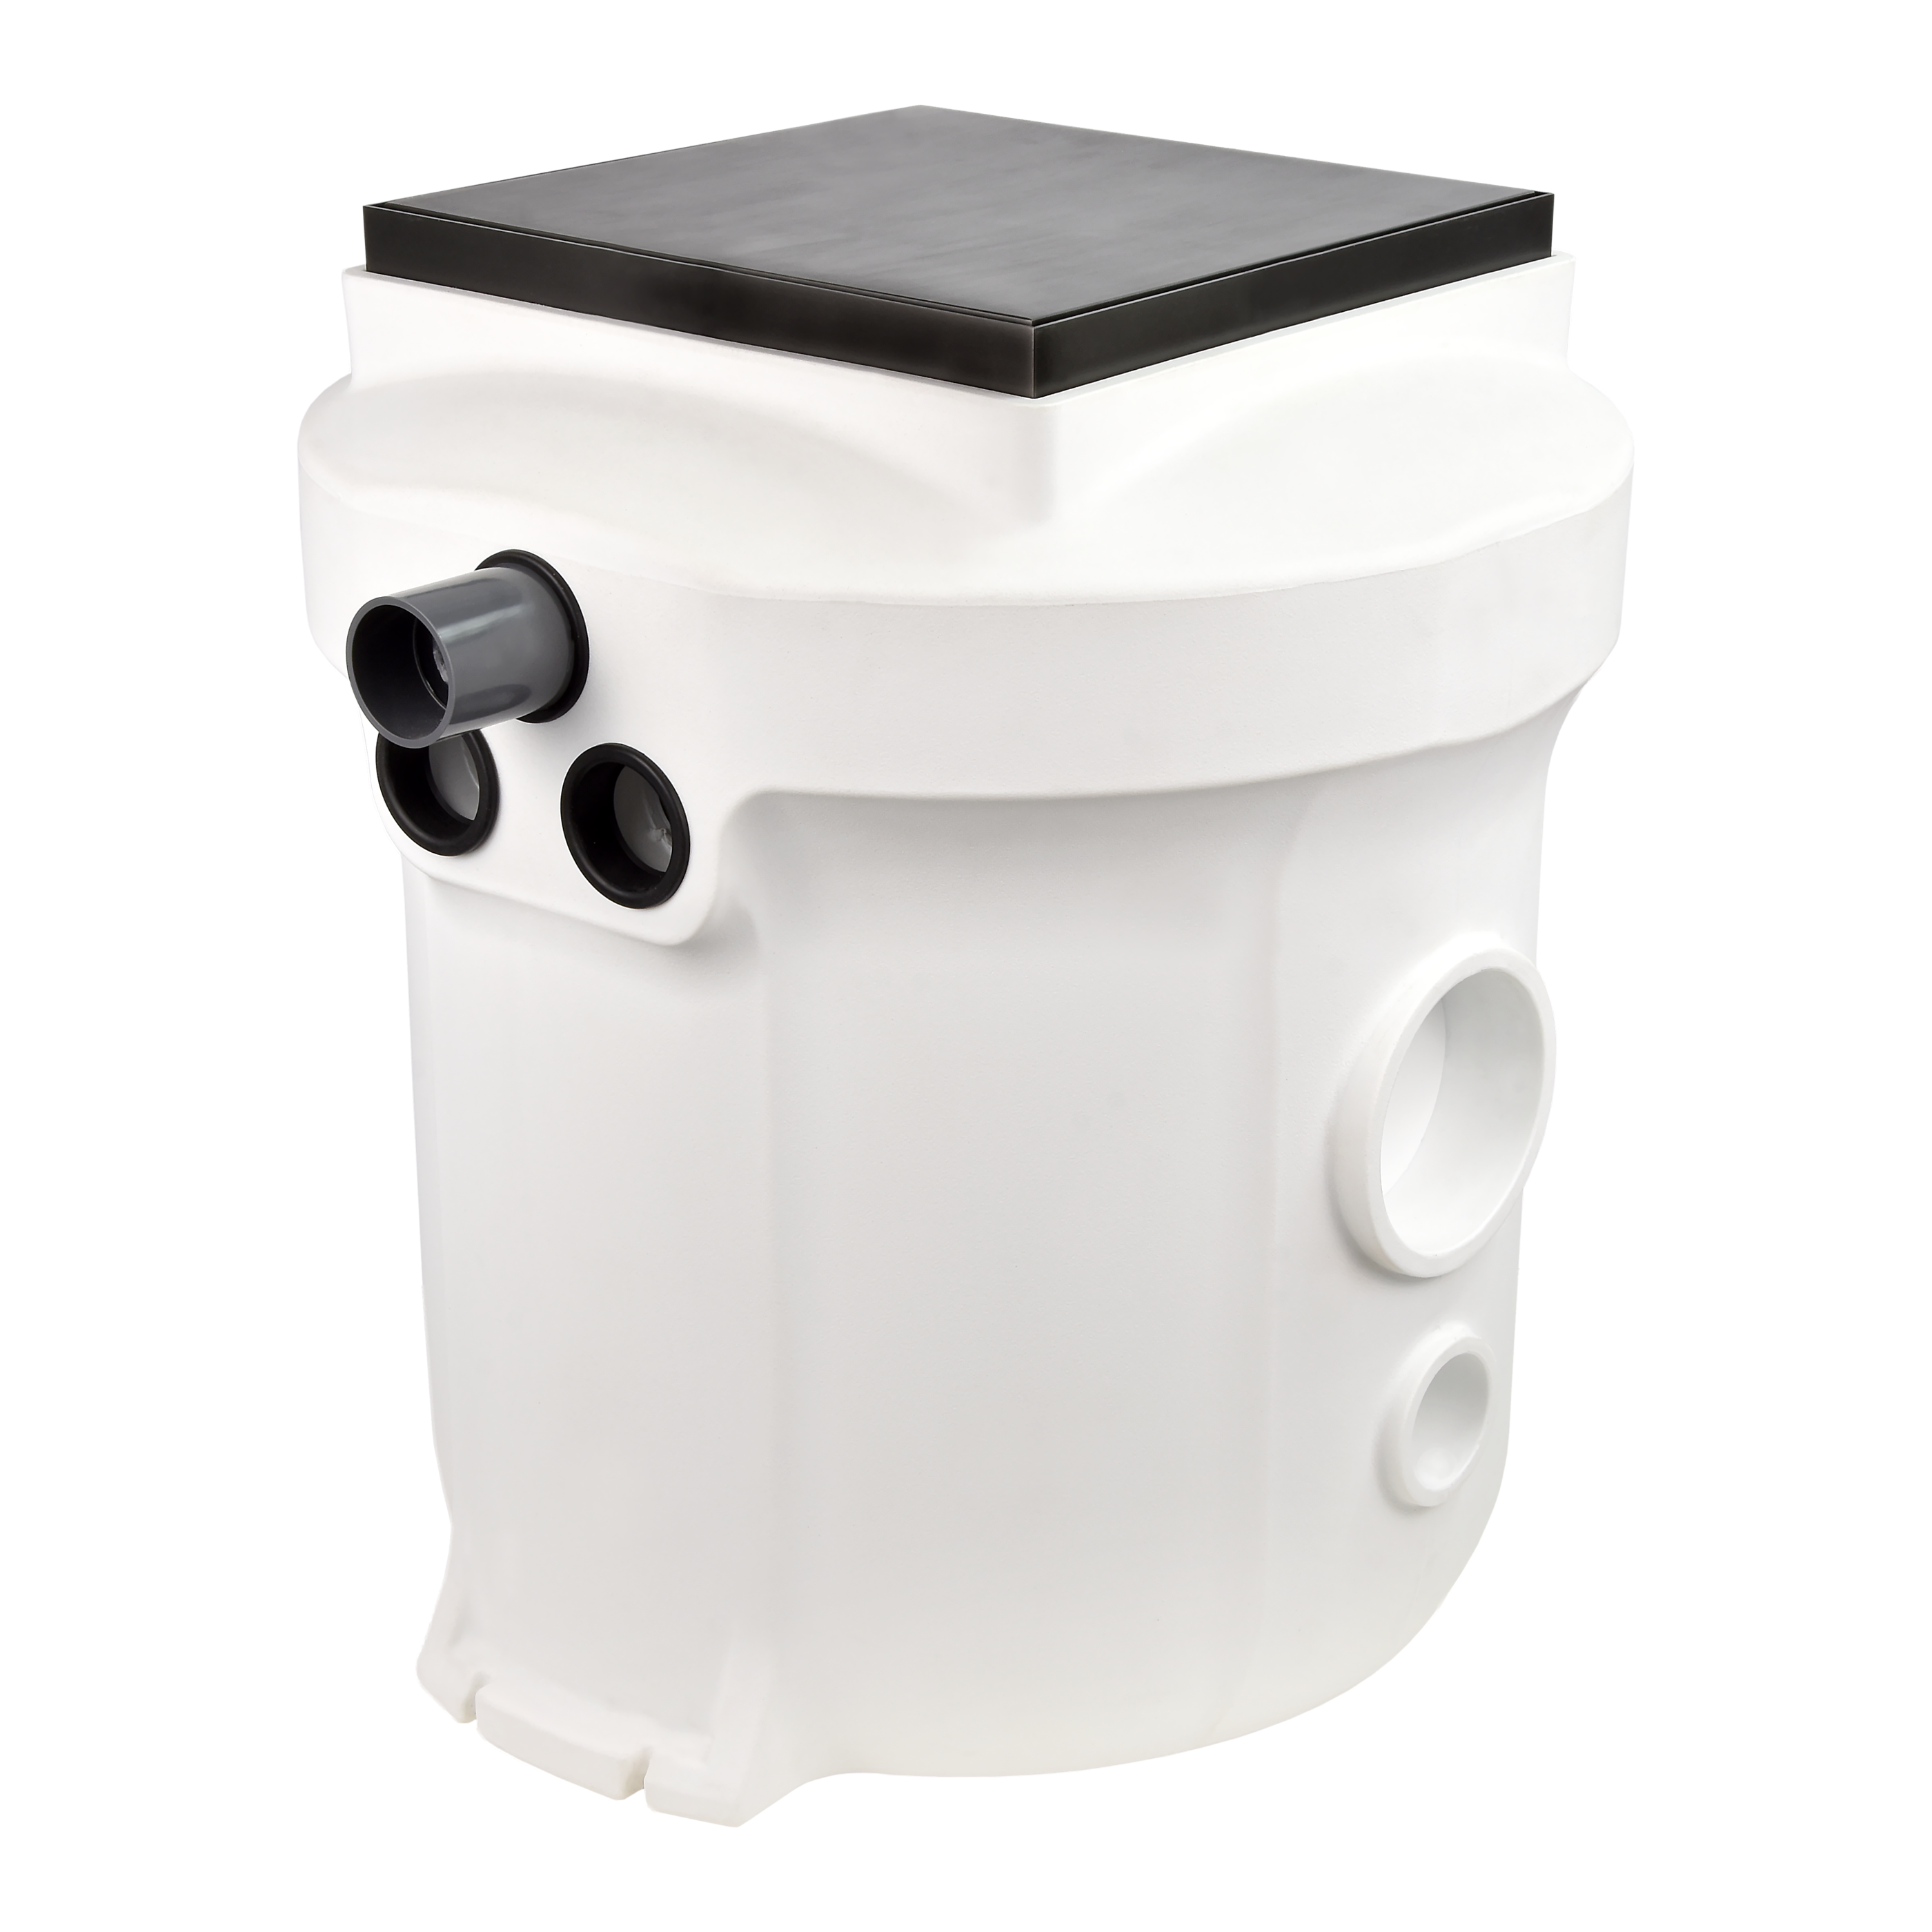
The SANBOX HB lifting station by IBO is a modern and reliable solution for lifting and transporting greywater and rainwater when gravity drainage is not possible. It is designed for underfloor or freestanding installation in single-family and multi-family residential buildings, as well as small commercial facilities.
The SANBOX HB lifting station is supplied as a complete, ready-to-install 150 l underfloor tank, equipped with 2 single-phase pumps, PVC fittings (check valves and a shut-off valve), and a SANBOX controller to which the pump power cables and the level sensor's air hose must be connected.
Key features of SANBOX HB:
- Suitable for collecting and pumping non-fecal wastewater.
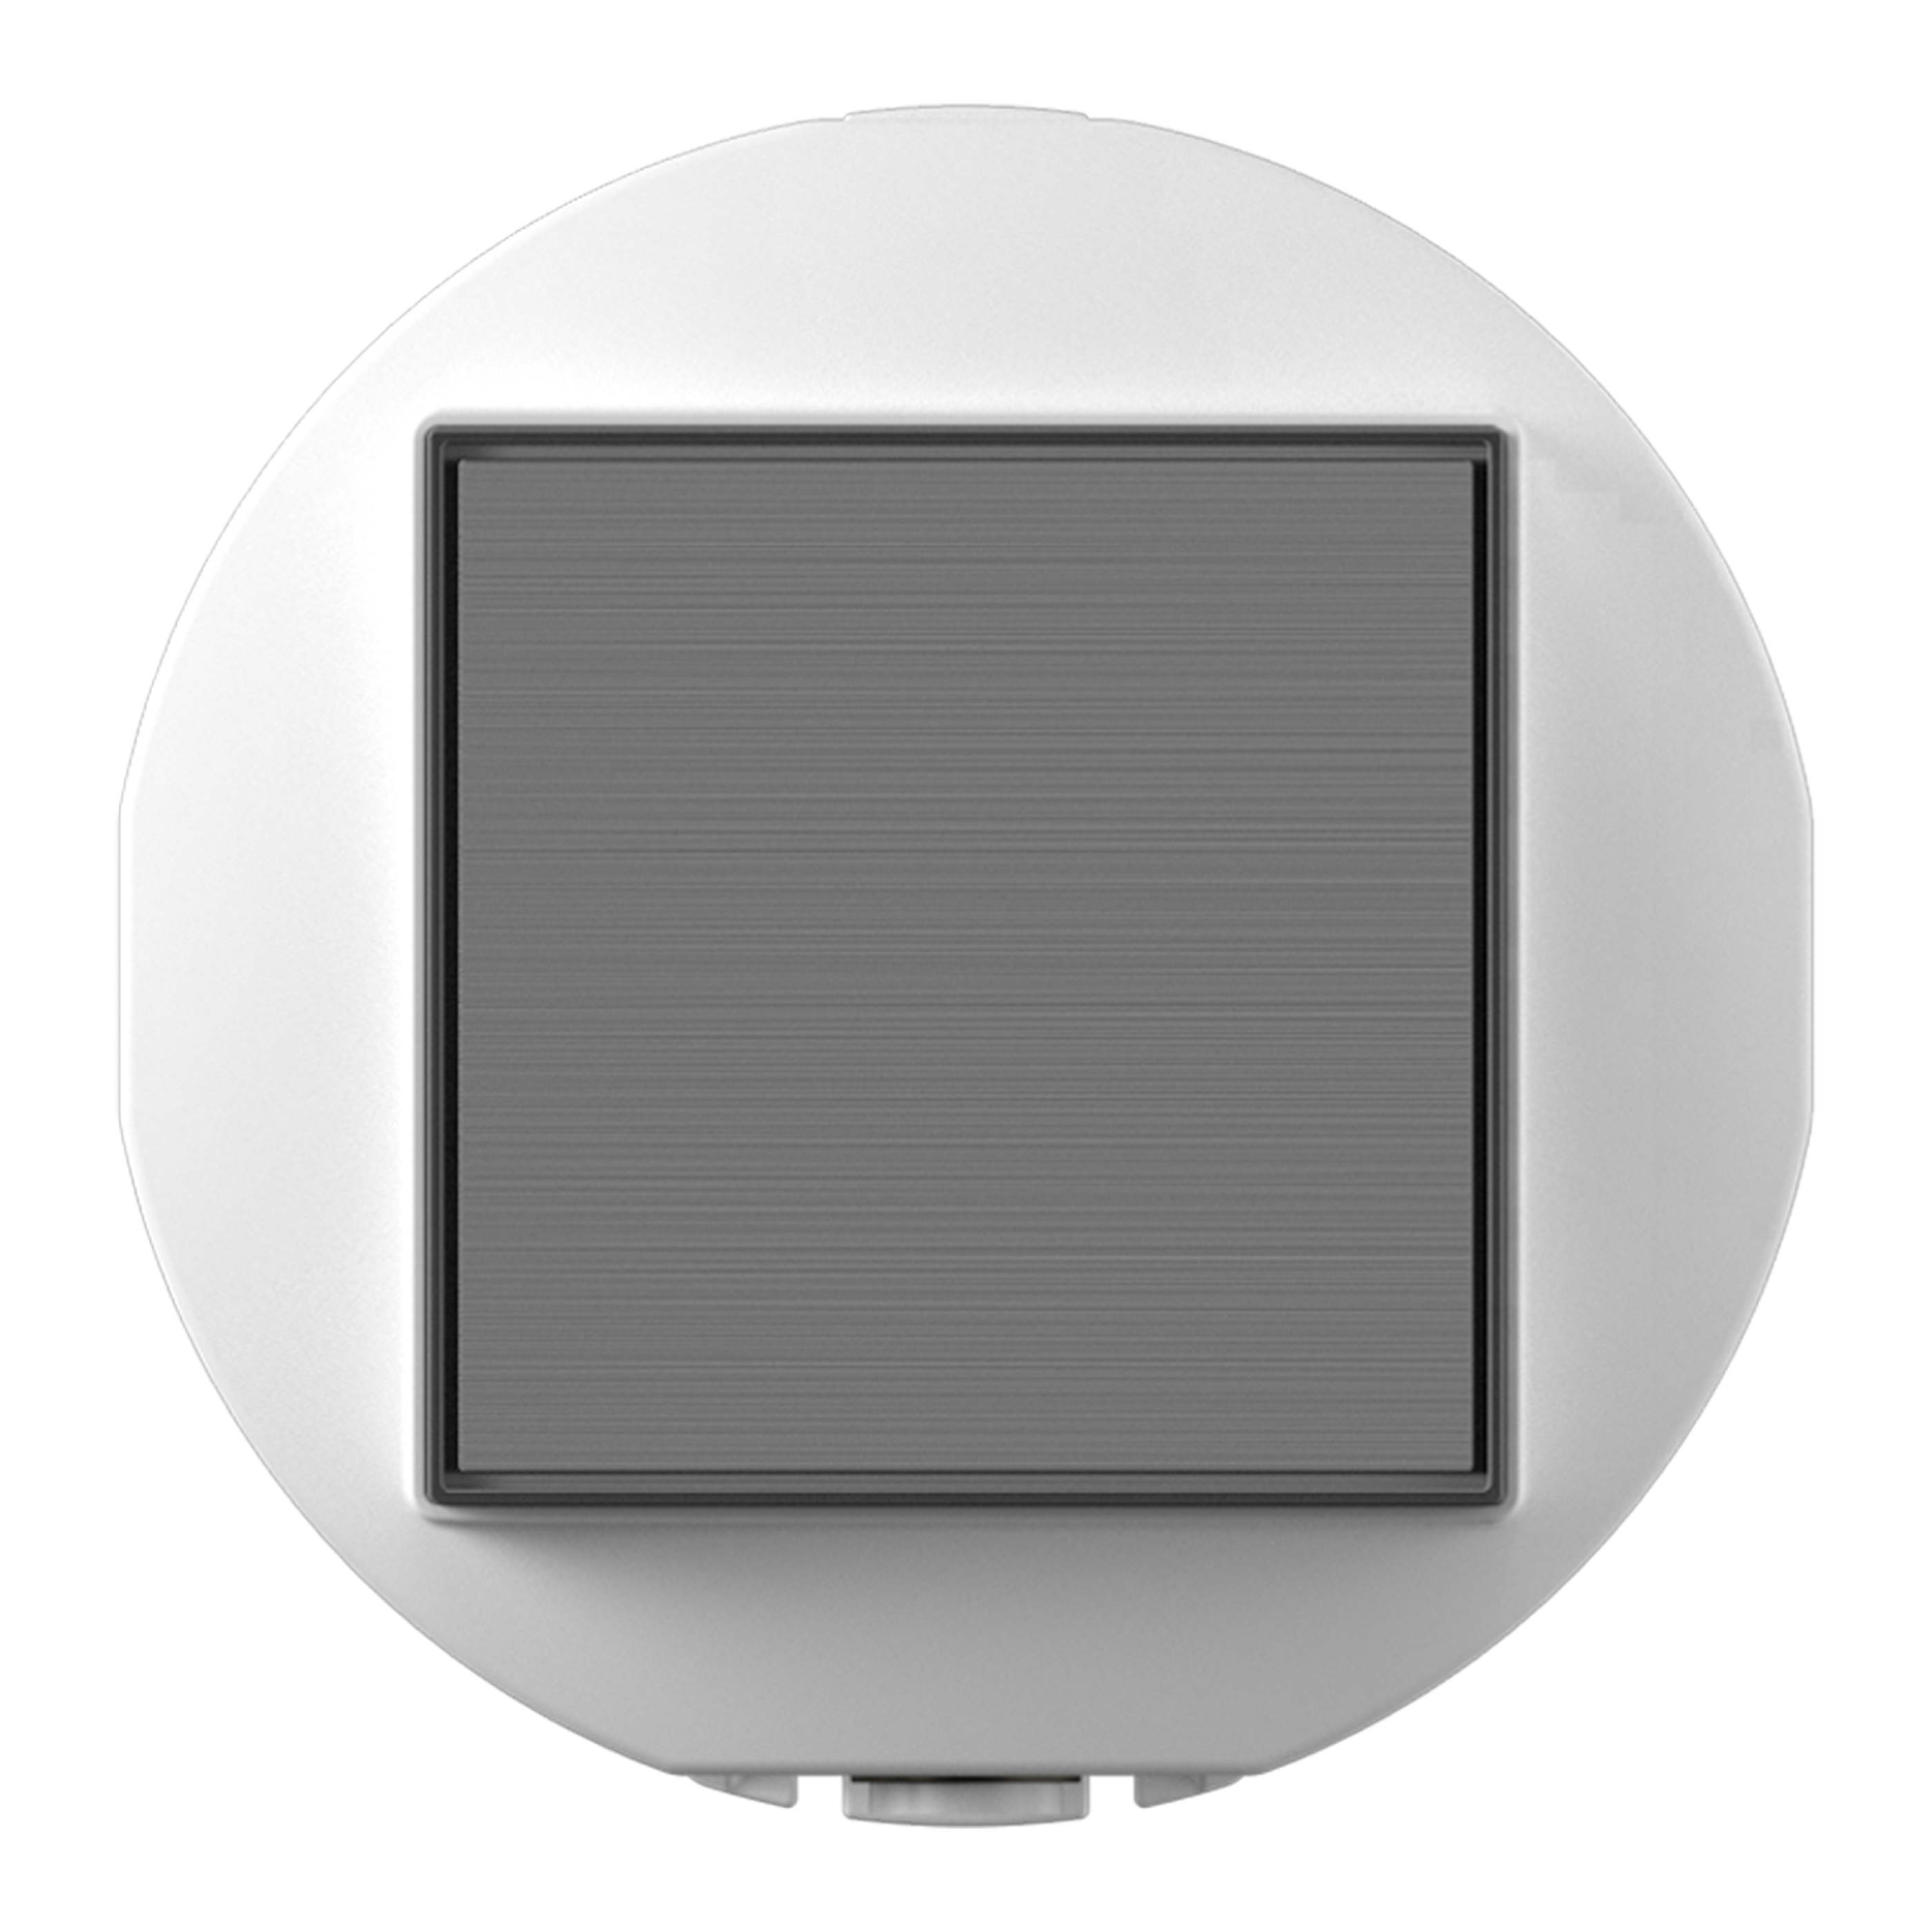
- Modern stainless steel cover with an attractive appearance and a load capacity of up to 150 kg (it can serve as a 35 × 35 cm floor drain grate).
- Two high-quality AISI 304 stainless steel submersible pumps, oil-cooled, ensuring quiet and trouble-free operation.
- Free passage for particles up to 25 mm in diameter – ideal for greywater, rainwater, flat-surface drainage, and discharge from kitchens, laundries, or spas.
- Advanced wastewater level control using electronic pressure sensors (0–10 kPa pressure switch), with network operation, remote monitoring, and alarm diagnostics.
- Optional automatic backwash system – effectively prevents impurities from settling on the tank walls.
SANBOX HB scope of supply:
- 150-liter PE tank
- Square stainless steel cover
- 2 submersible pumps with motors (VORTEX type)
- 2 check valves
- Drainage and venting kit
- Complete controller with electronic pressure switch and level sensor
- Standard accessory set: flexible hoses, sealing rings
- Documentation: operating manual, CE declaration
Optional equipment:
- Backwash kit with rotating nozzle and automatic control
SANBOX HB technical data:
| Model |
SANBOX HB 2x750 |
| Motor power |
2 x 0,75 kW |
| Current |
3.1 A |
| Max. head |
12 m |
| Max. capacity |
18 m³/h |
| Free passage |
25 mm |
| Tank capacity |
150 liters |
| Weight |
65 kg |
| Protection class |
IP68 |
| Motor cooling |
Oil-cooled |
| Operating mode |
S1 (continuous operation) |
| Discharge outlet |
1x d63 (horizontal) |
| Vent |
1x d50 |
| Cable gland |
1x d50 |
| Inlet outlets |
3x d110 |
| Inlet outlets |
3x d50 |
Materials:
-
Tank: PE (polyethylene)
-
Motor housing: AISI 304 stainless steel
-
Impeller: Cast iron
-
Motor shaft: AISI 304 stainless steel
-
Oil chamber: Cast iron
-
Sealing: NBR, SiC mechanical seal
-
Check valves: Fiberglass-reinforced composite
-
Fittings: AISI 304 stainless steel
-
Dimensions: 620/540/550 mm
Benefits of choosing SANBOX HB:
- Reliable removal of greywater and rainwater
- Quiet and safe operation thanks to oil-cooled pumps
- Remote control and monitoring capability
- Solid construction and modern design
- Optional flushing system that keeps the tank clean
SANBOX HB pumping stations by IBO are a reliable and functional solution designed for demanding users. They ensure comfort and safety during everyday operation. Please note that SANBOX HB is not intended for removing wastewater from toilets.
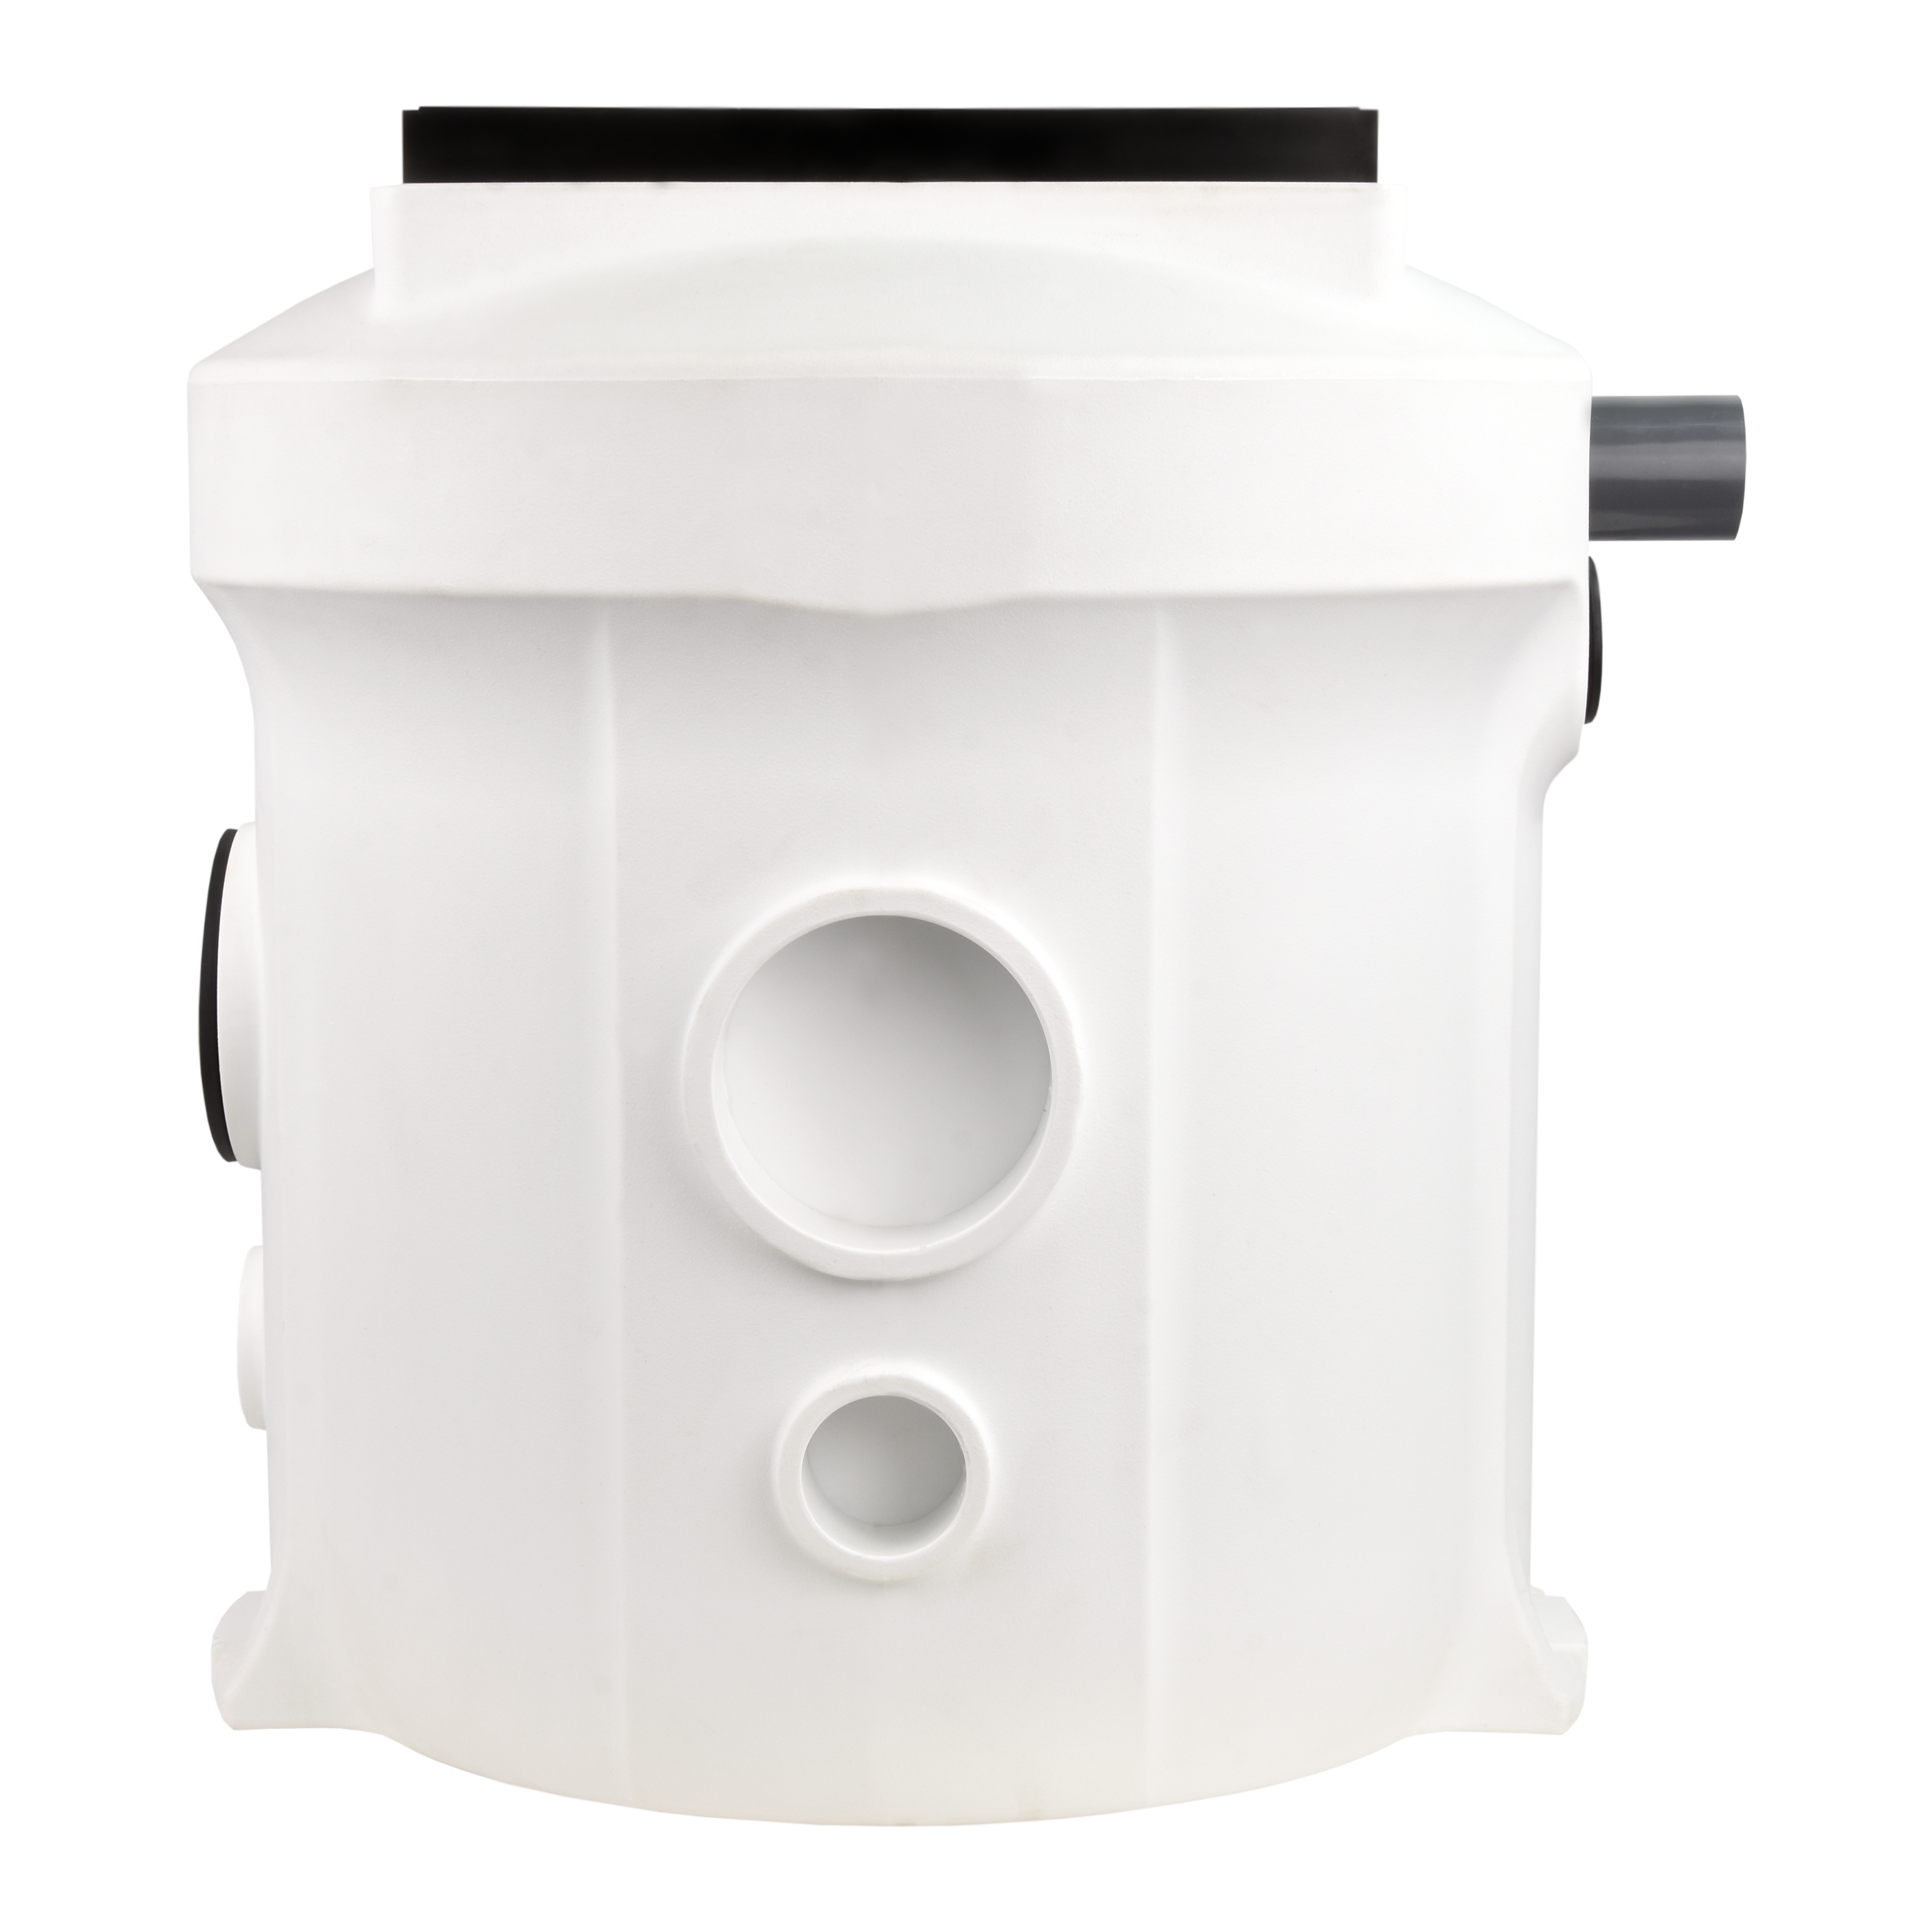
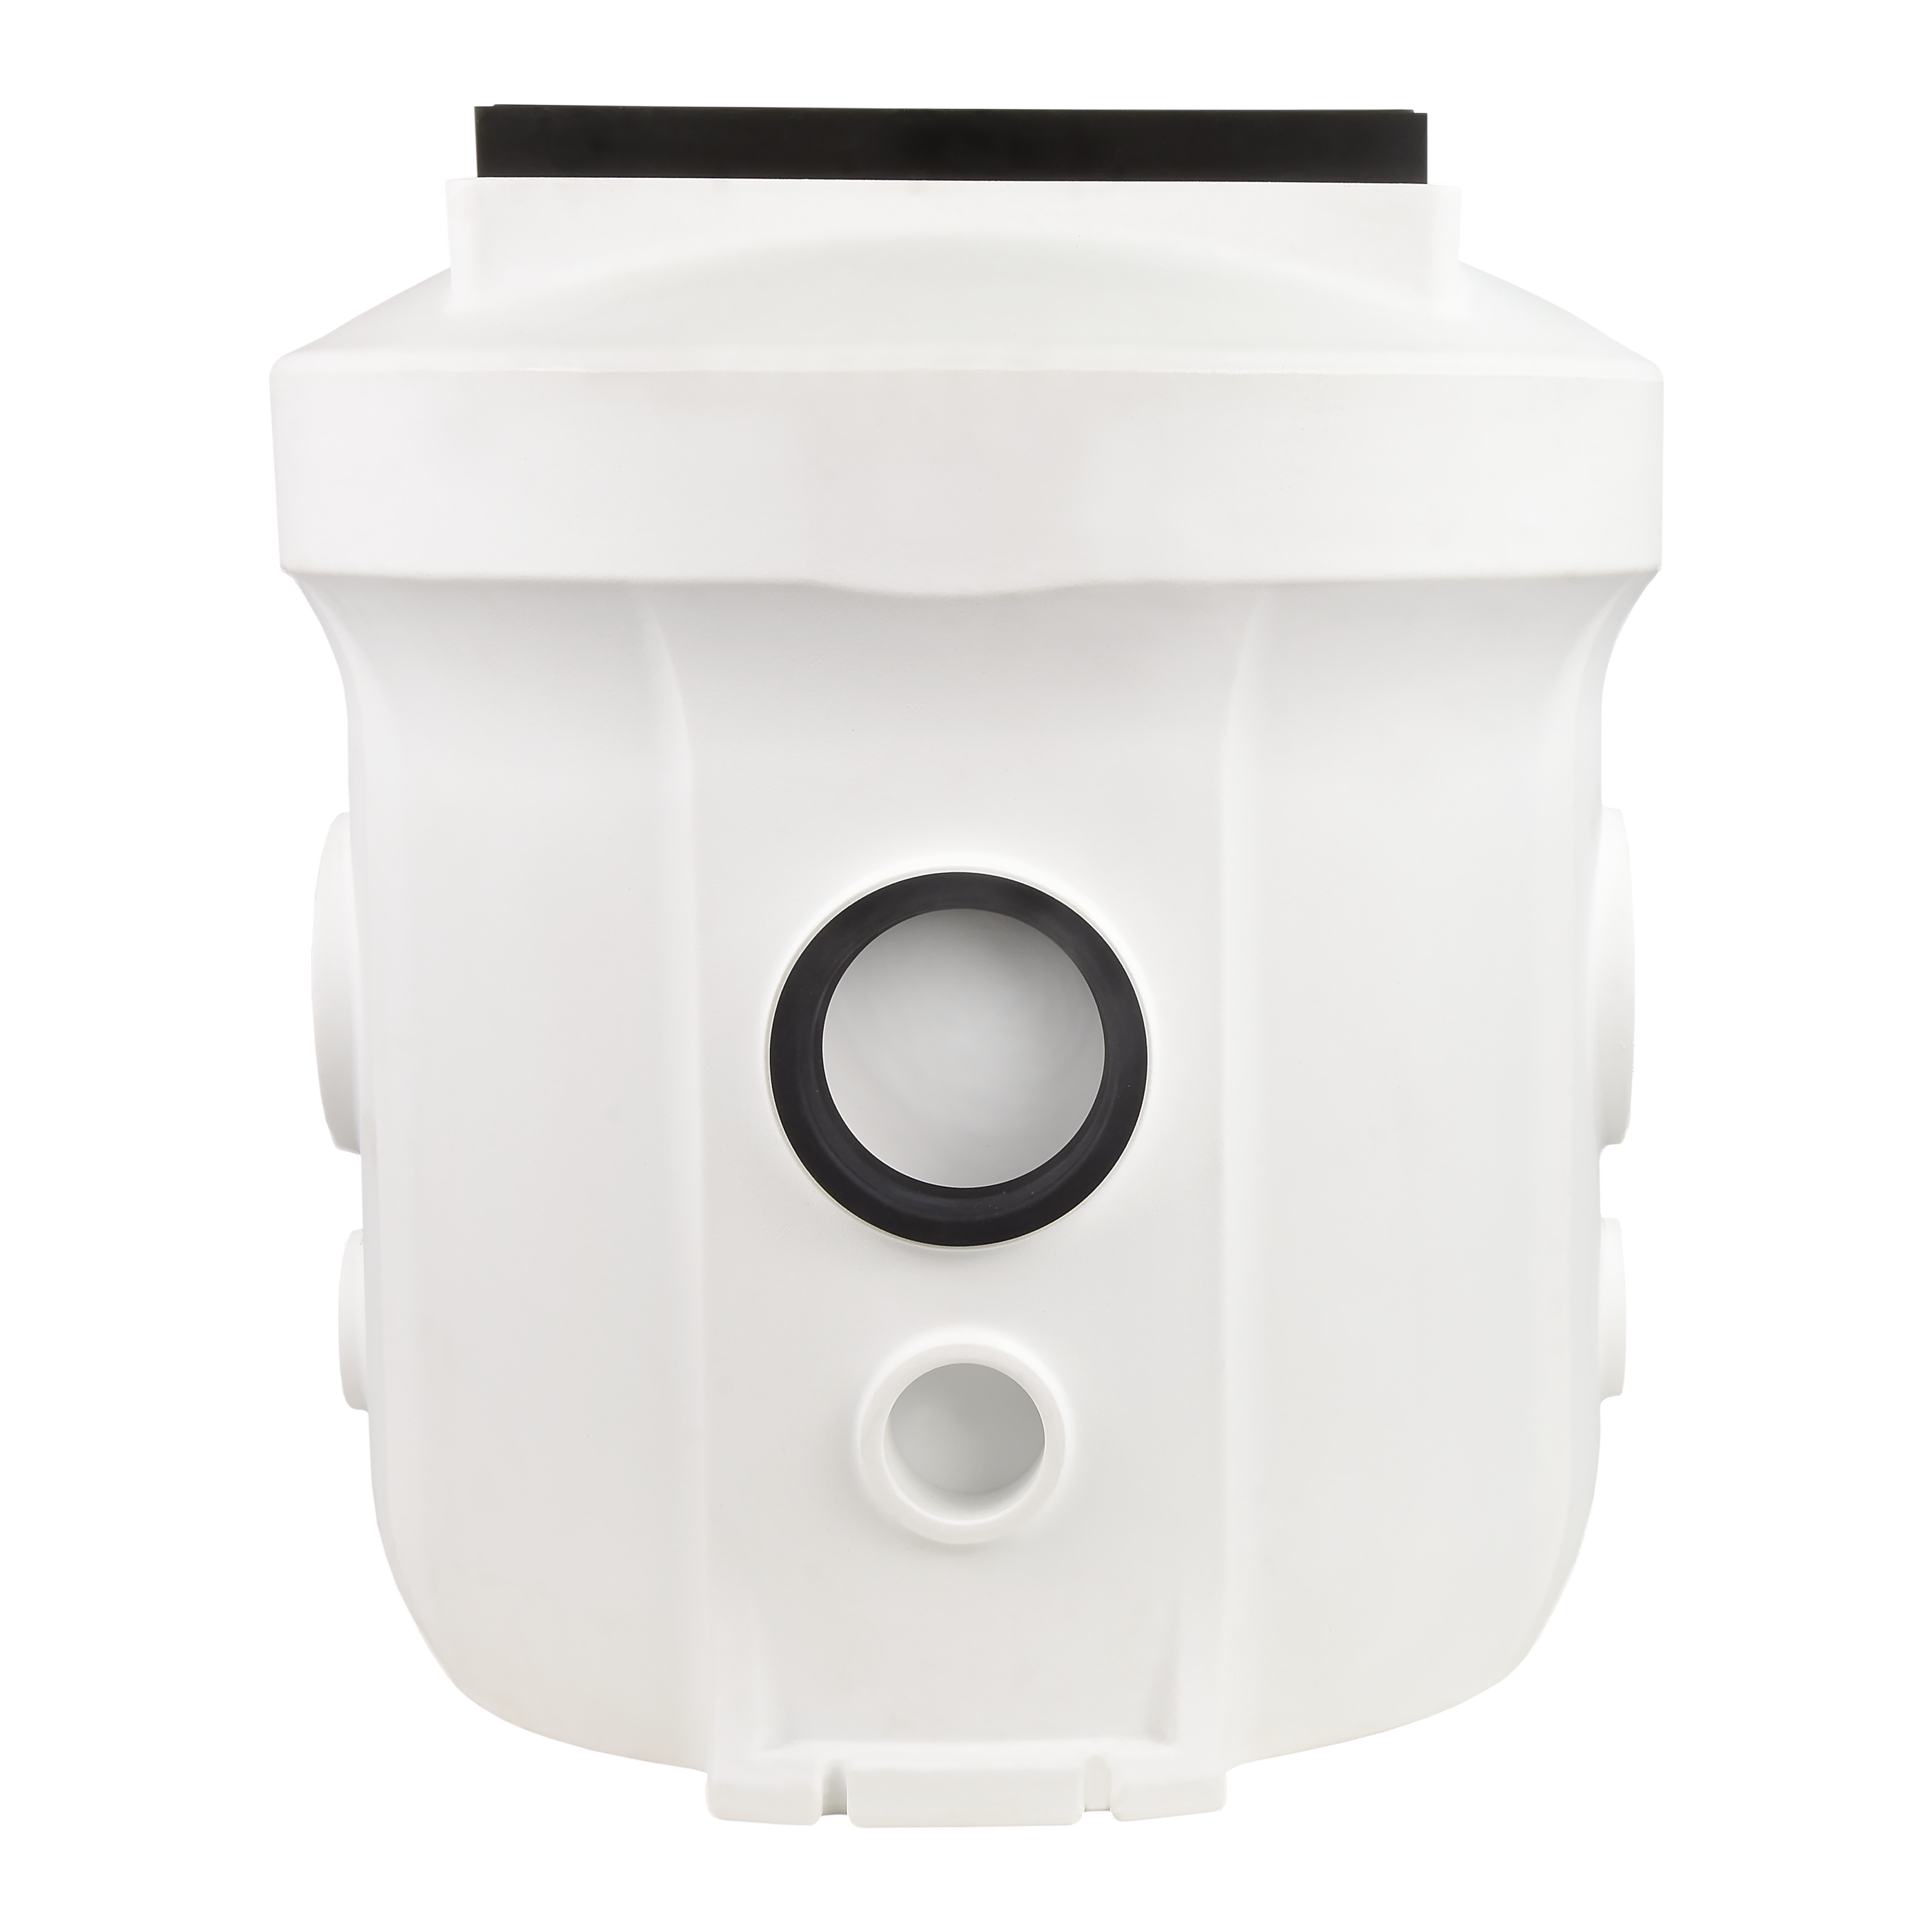
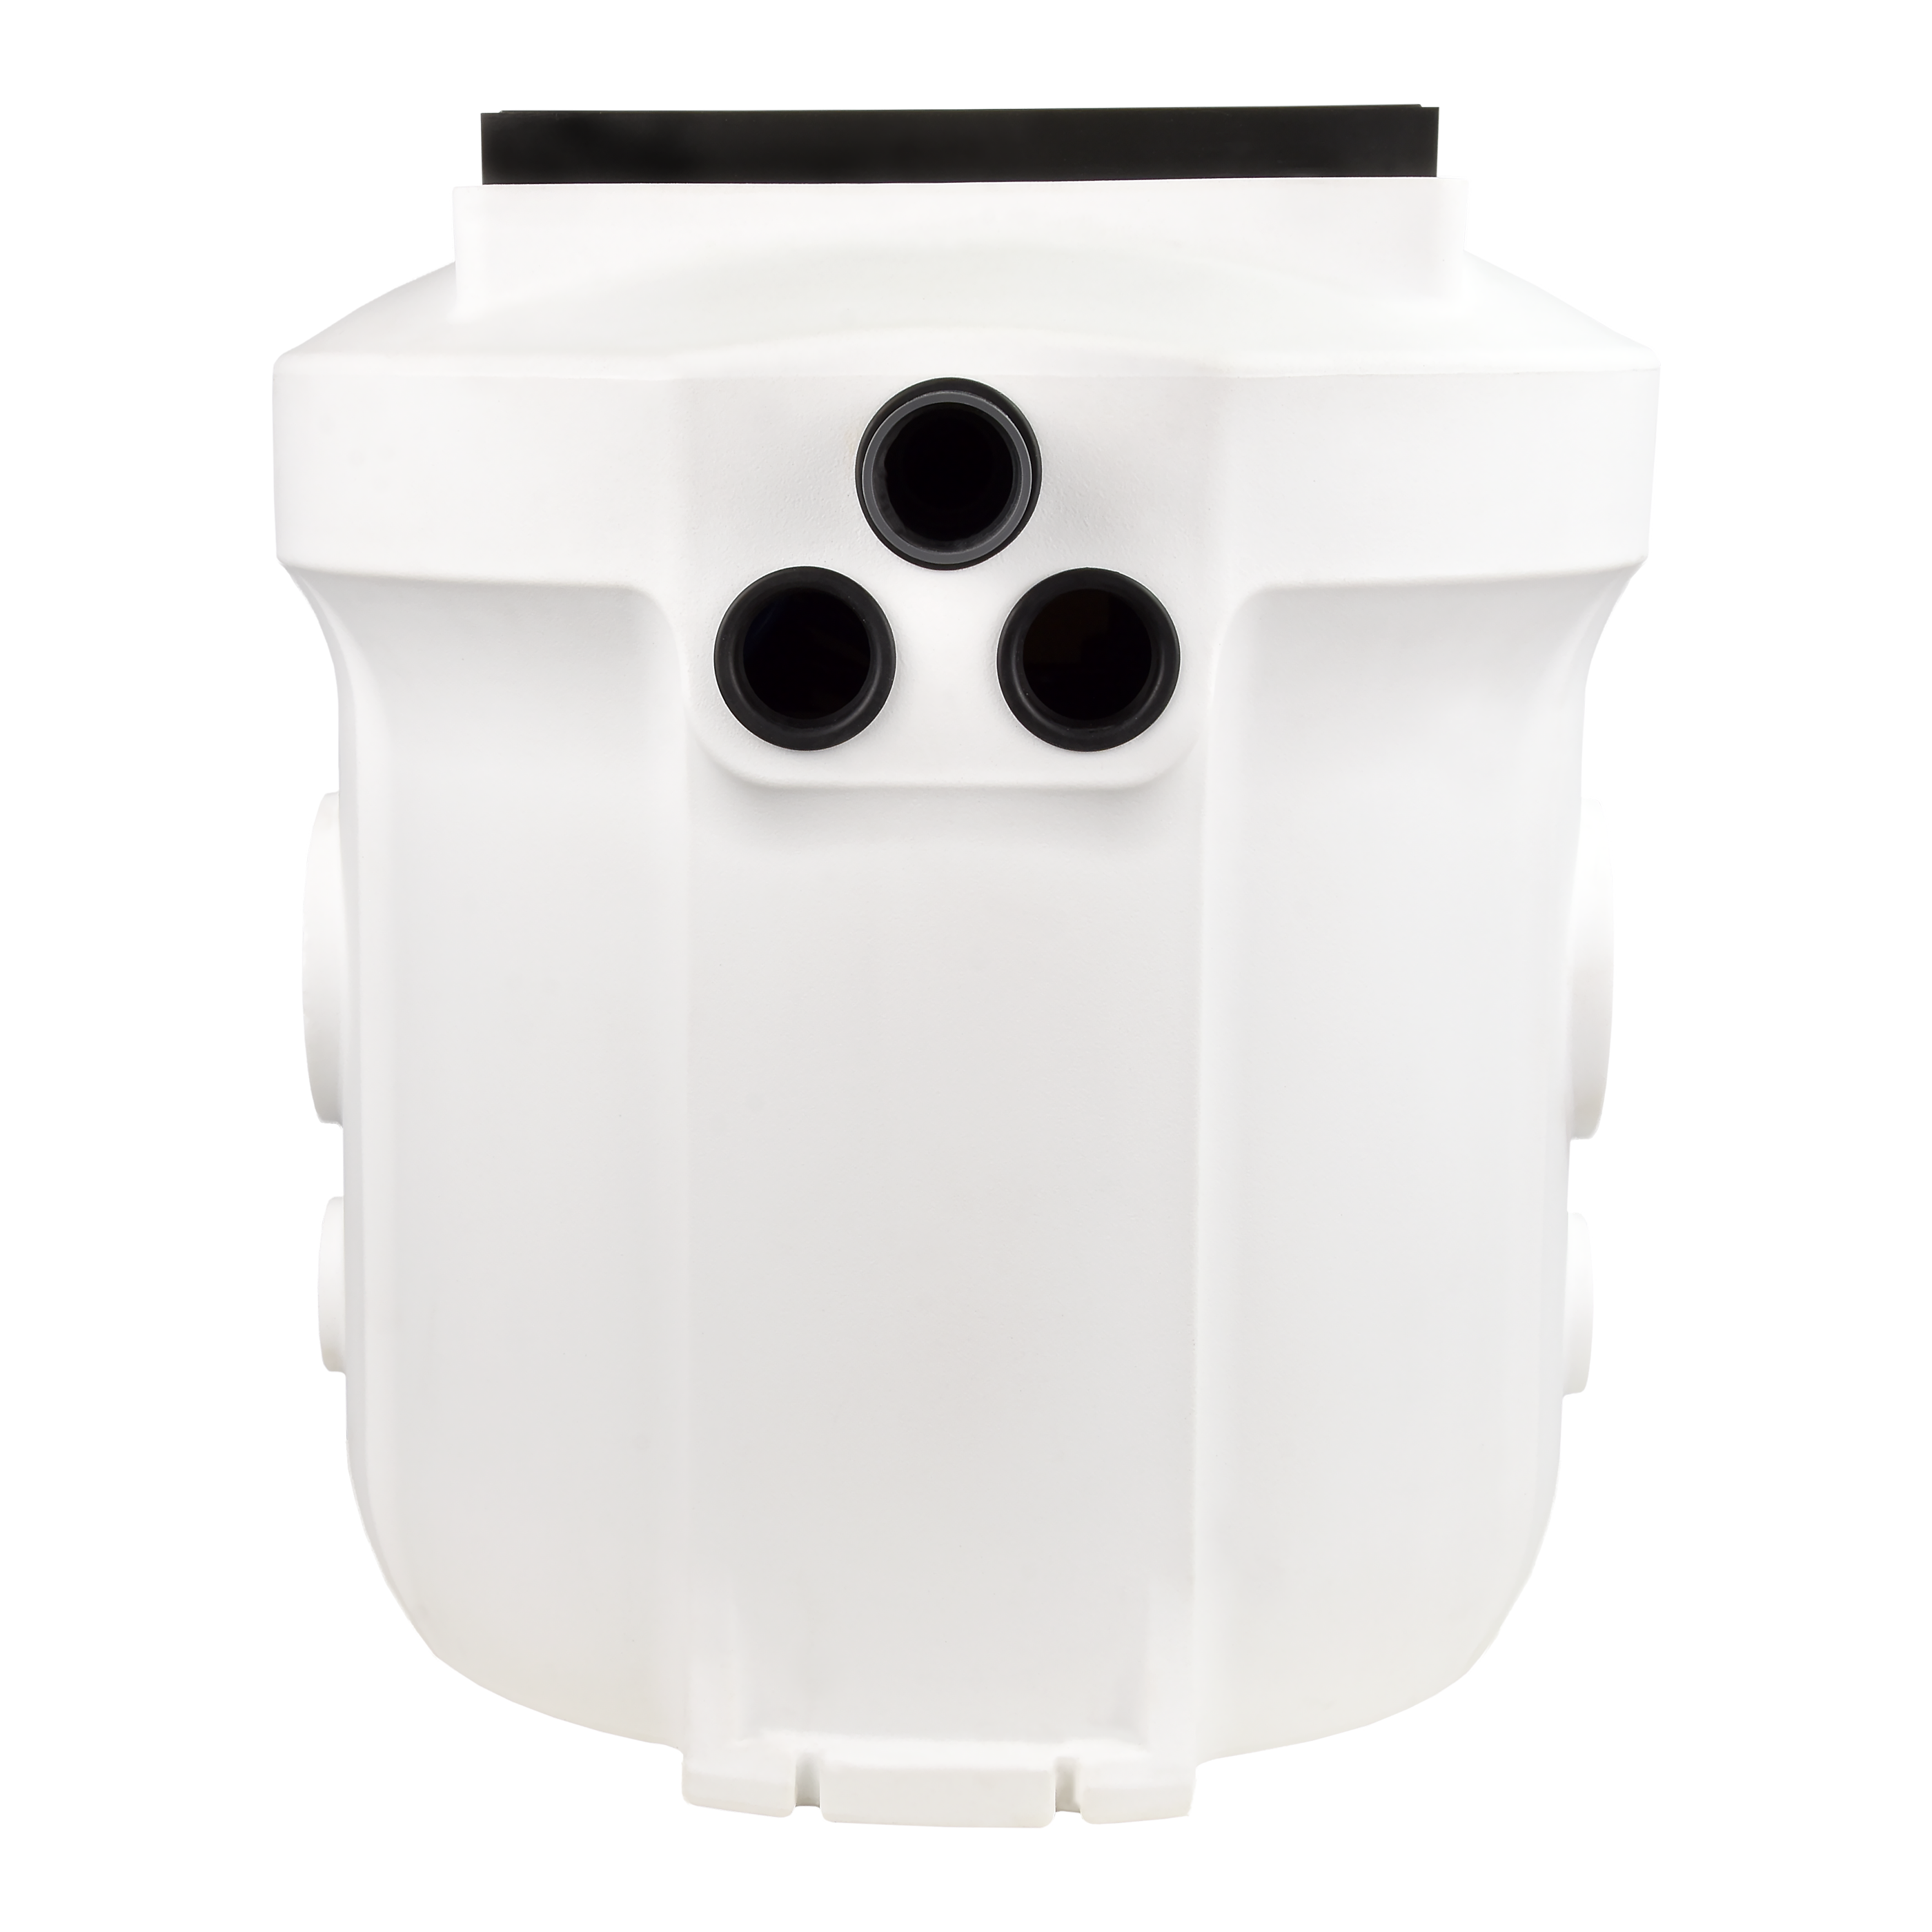
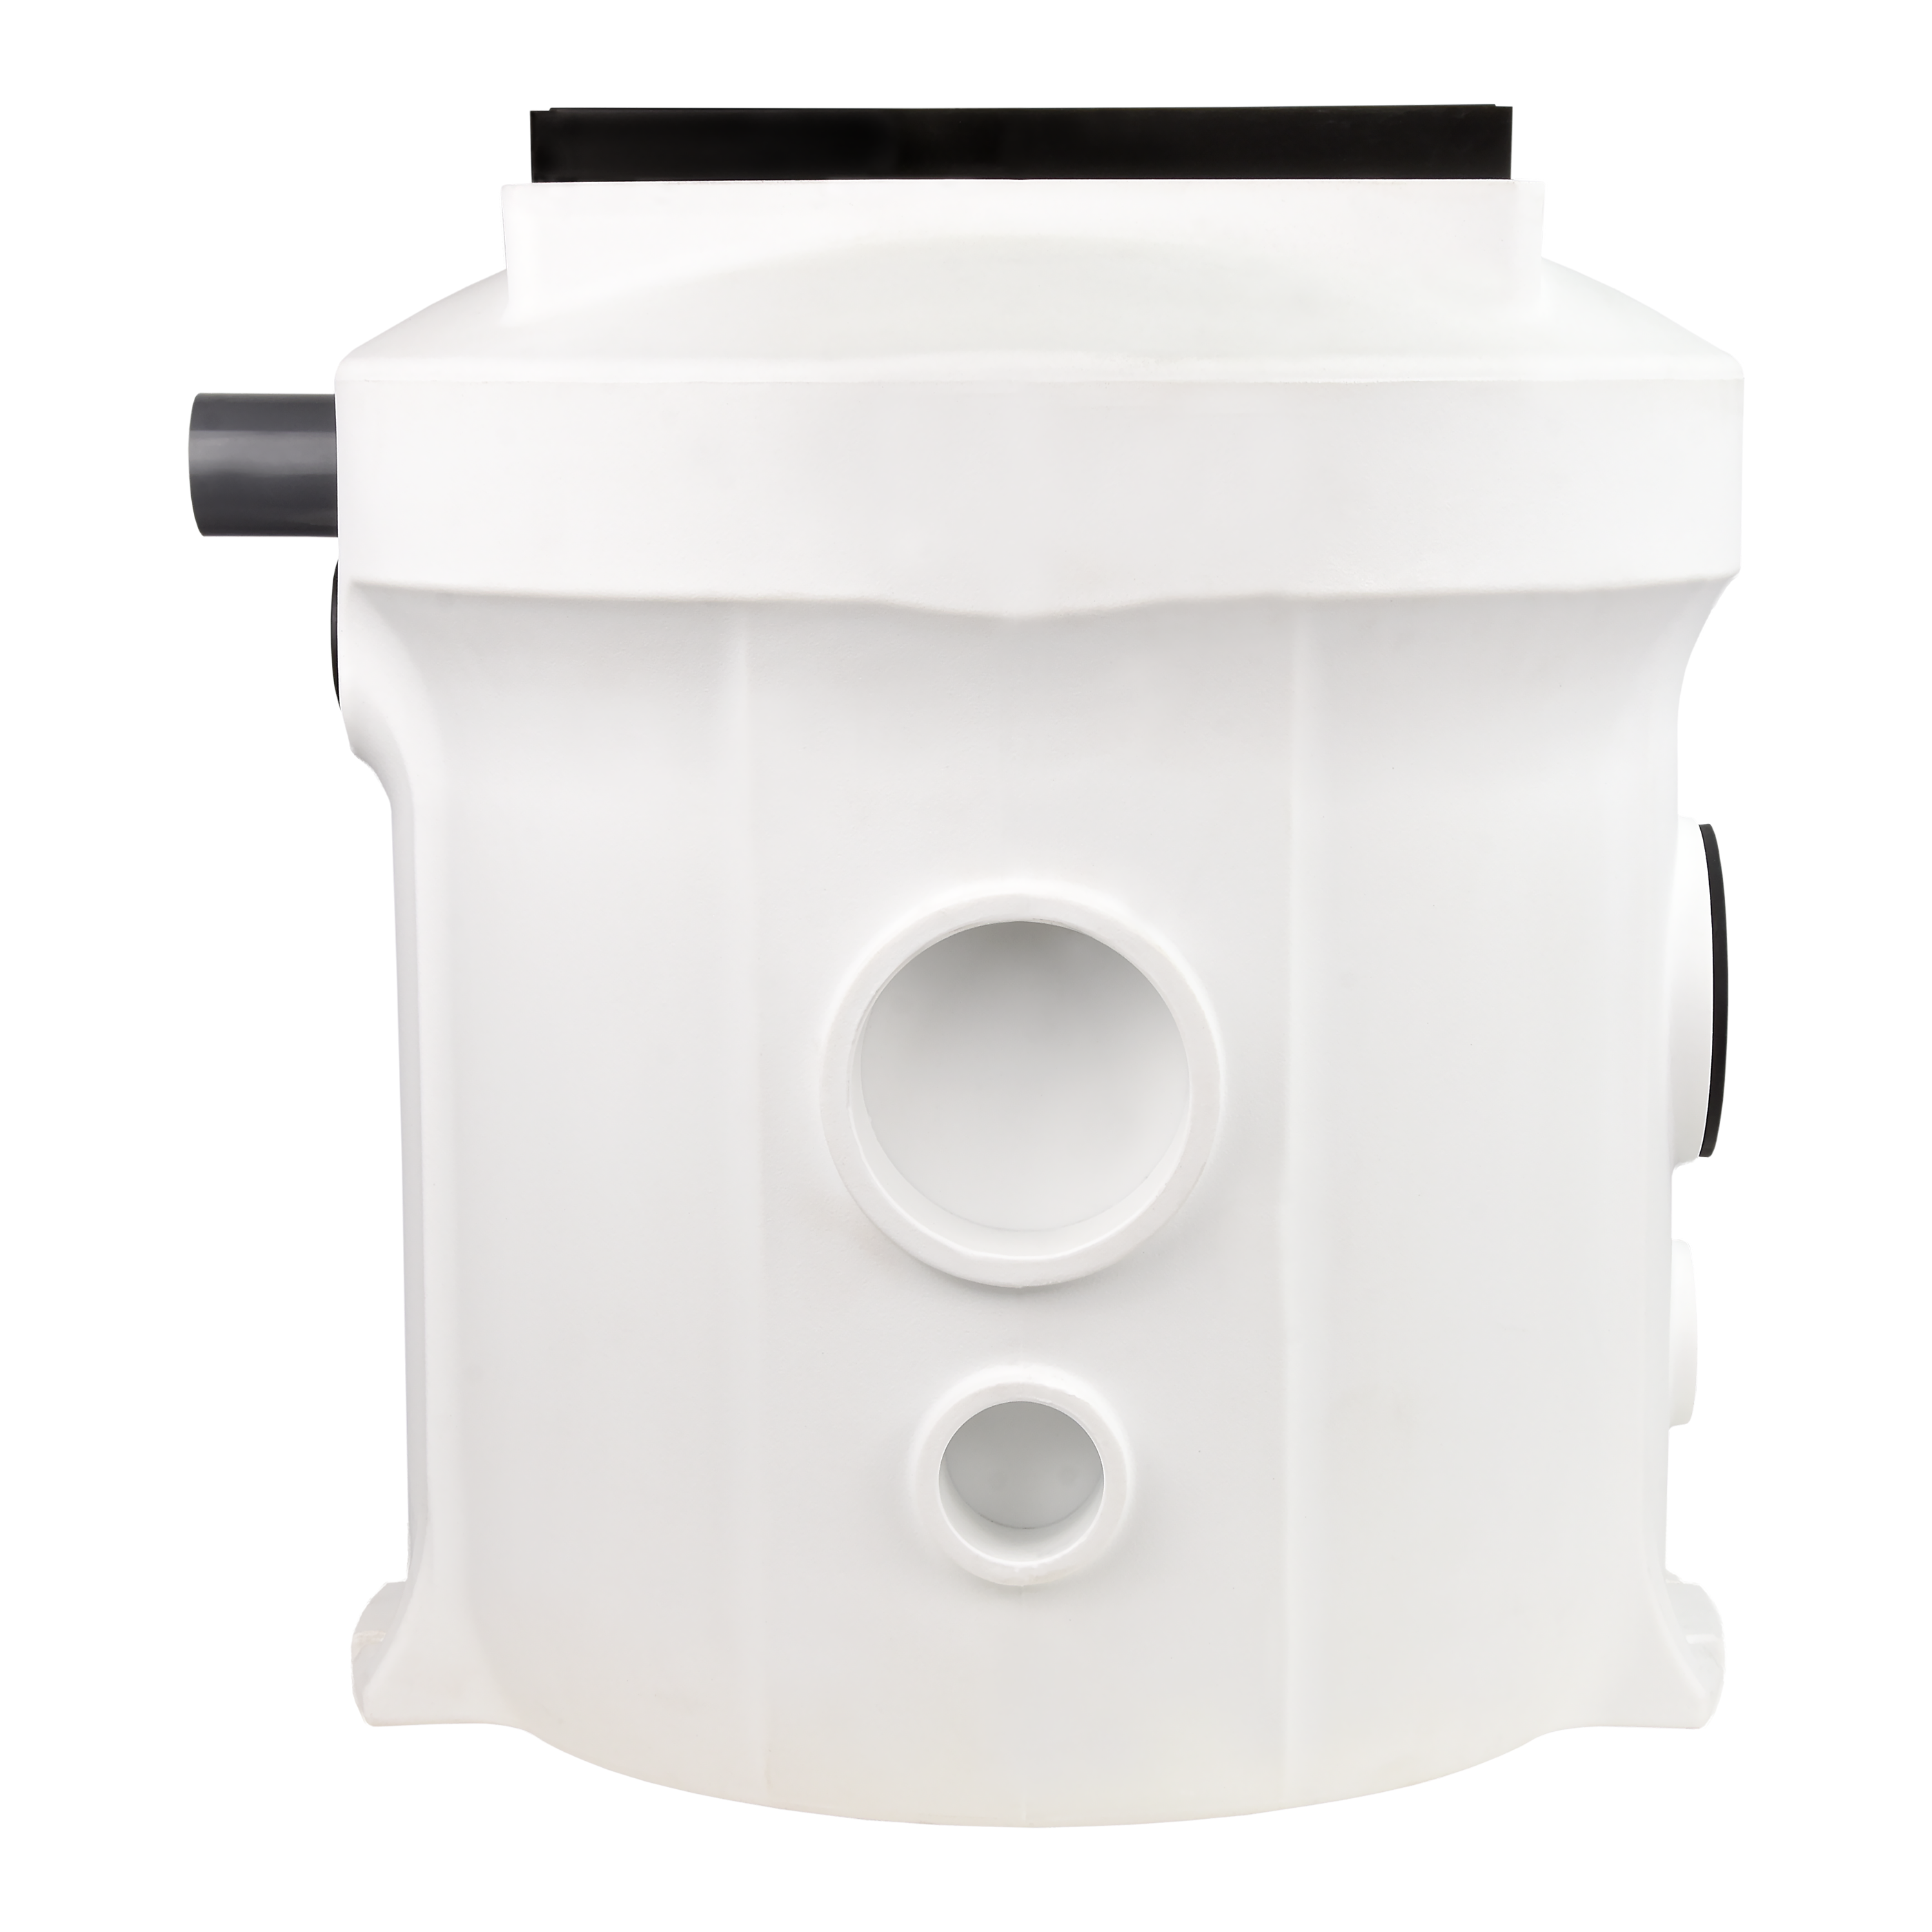
The 150-liter pumping station tank allows connection of up to 3 D110 gravity inlets and up to 3 D50 gravity inlets. It also features a D50 mm vent and a D63 mm discharge outlet.
The wastewater level in the tank is controlled using electronic pressure sensors that provide precise and reliable monitoring. The advanced SANBOX HB pumping station controller enables not only network operation, but also remote control and alarm diagnostics, increasing convenience and safety of use.
SANBOX HB smart controller – advanced management of wastewater pumping stations
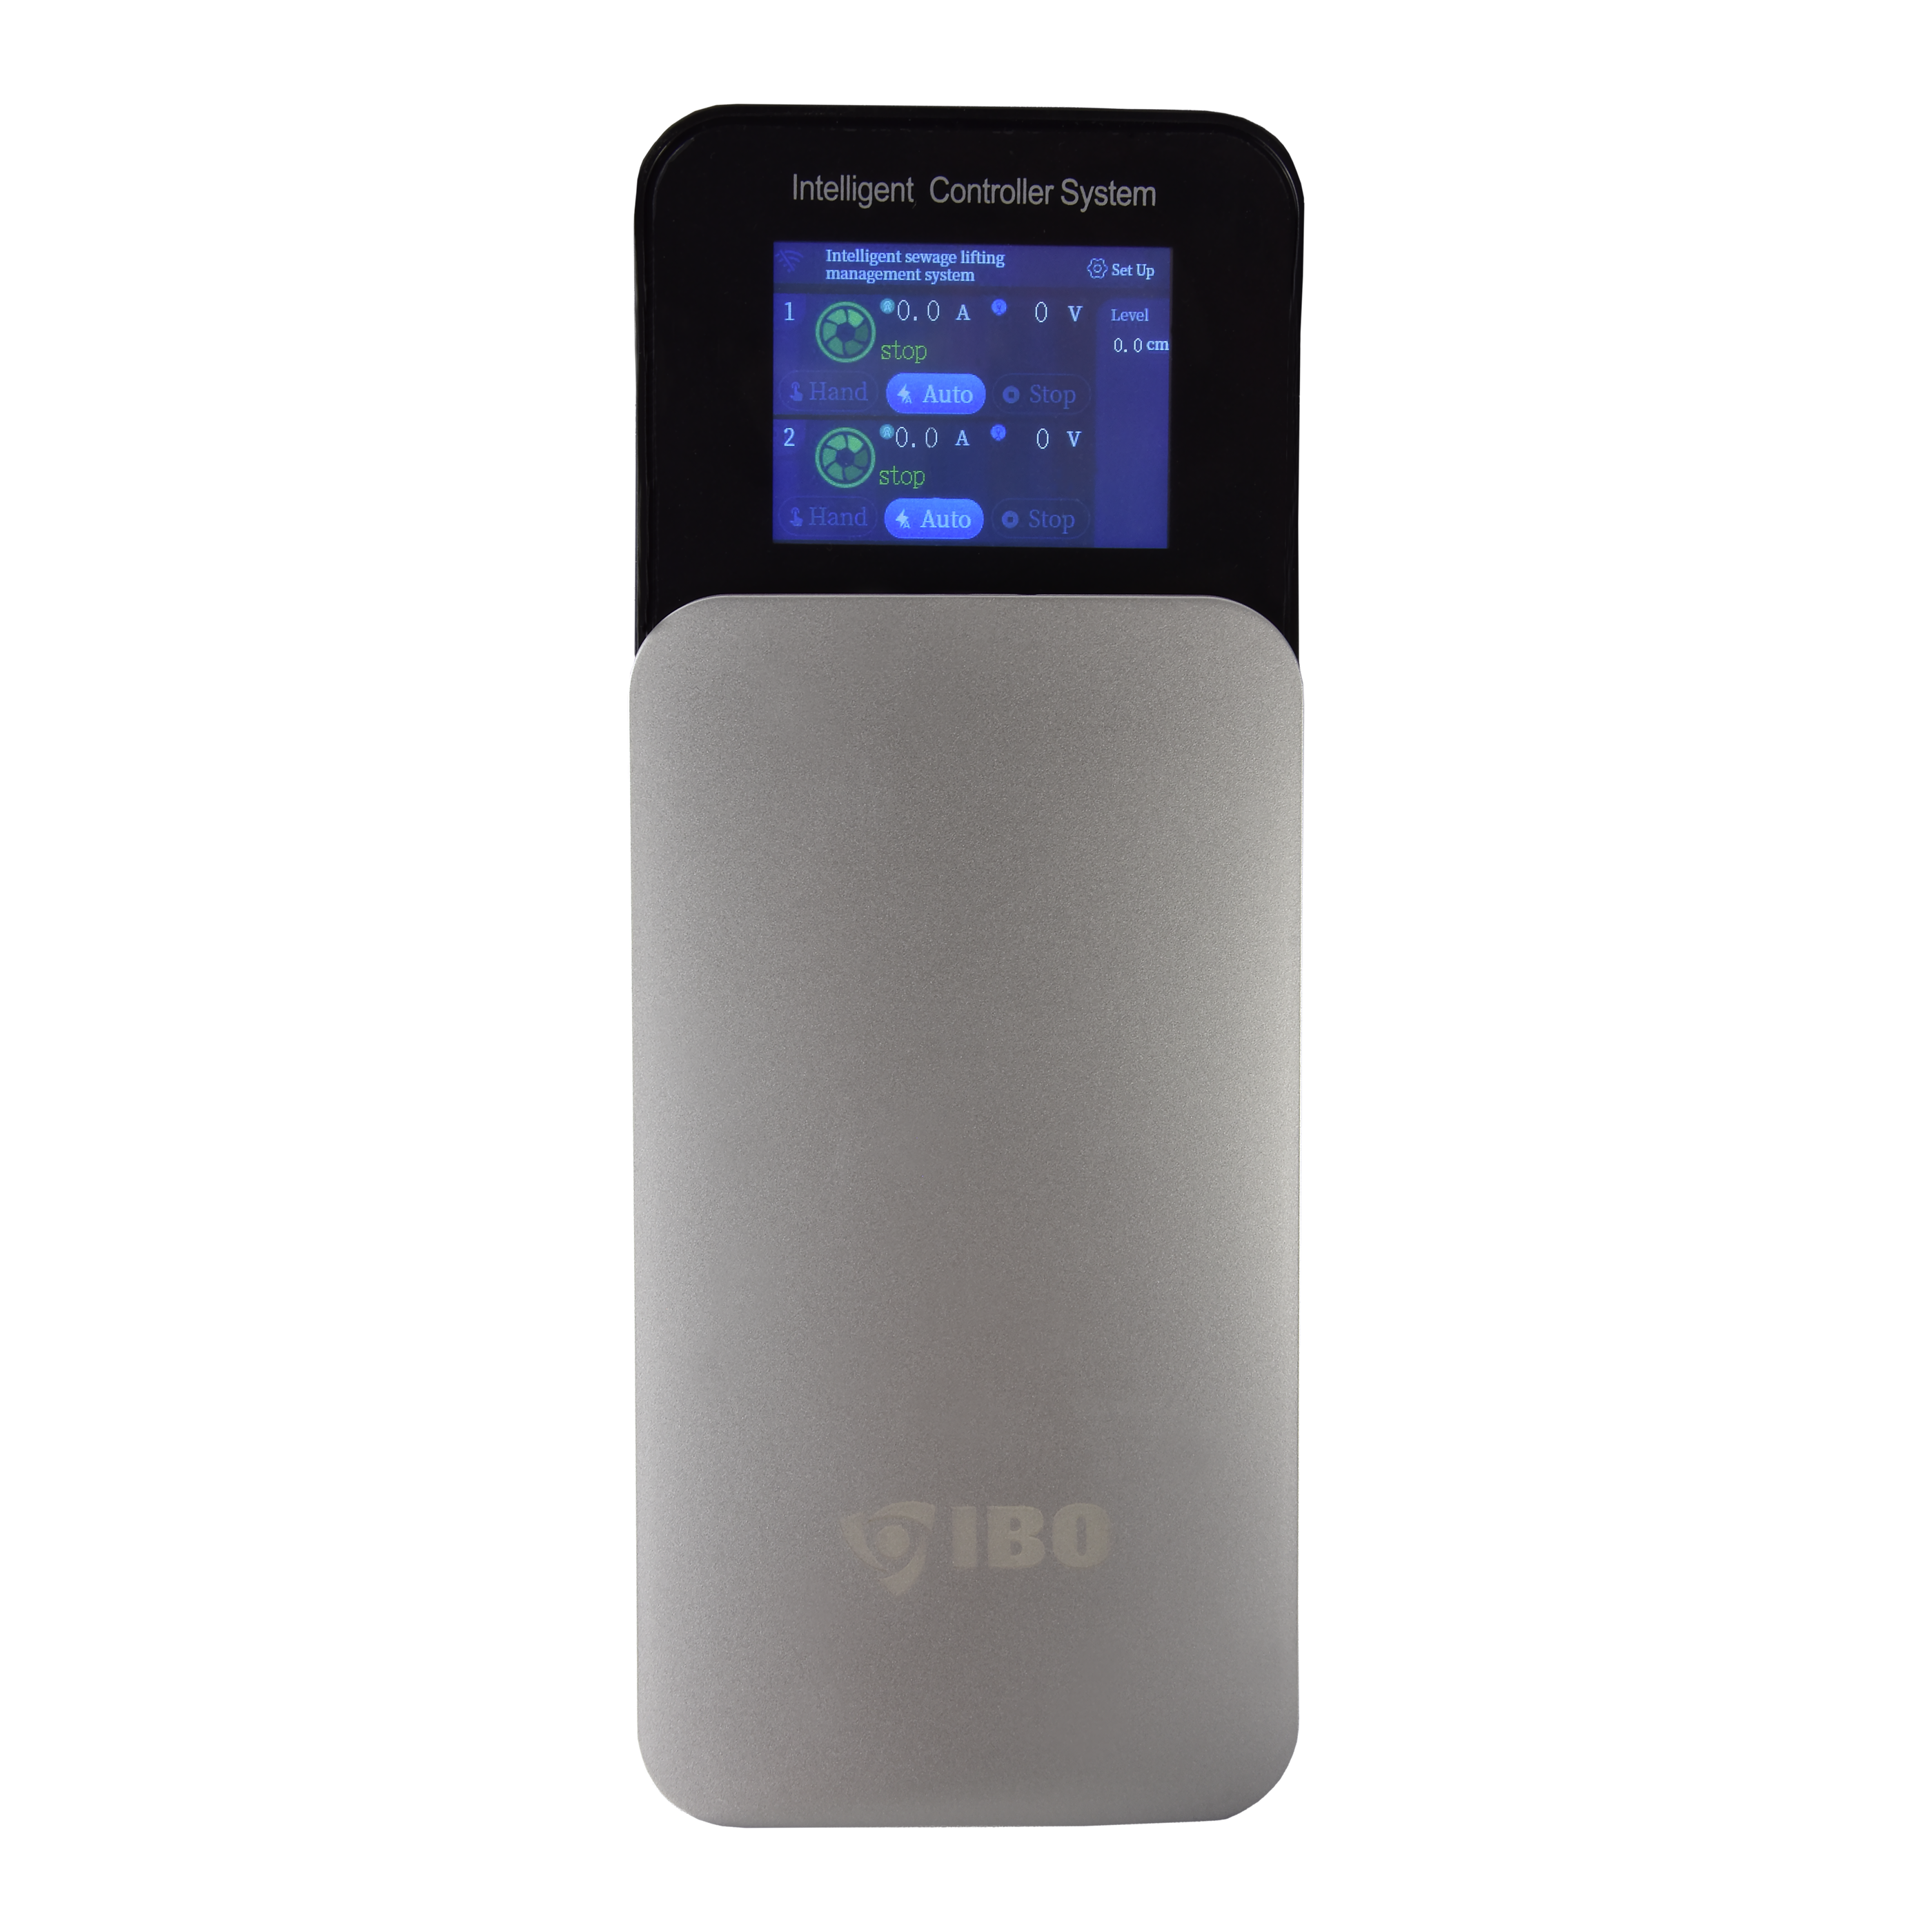
The intelligent SANBOX controller used in SANBOX HB pumping stations enables comprehensive monitoring and automatic sewage pumping by precisely controlling the liquid level in the pumping station tank. The measuring system is based on an electronic air pressure sensor, which sends a signal to the controller, enabling accurate determination of the current sewage level.
The controller allows the user to smoothly adjust key operating parameters, such as:
-
Operating liquid level (pump switch-on level)
-
Stop liquid level (pump switch-off level)
- Additional settings adapted to local conditions
This enables precise adjustment of system operation to the requirements of a specific application, ensuring reliability and fully automated management of the liquid level and pump motor operation.
The SANBOX HB controller is equipped with a range of advanced features that enhance safety and user convenience:
-
WiFi module enabling remote monitoring and control
- Water leak detection module
- Optional automatic tank backflushing module
The alarm system automatically reports critical conditions such as:
- High liquid level in the tank
- Dry running of the motor
- Motor failure or exceeding safe operating parameters
The controller also features:
- Motor current monitoring system
- Motor temperature monitoring system
-
Safety circuit with delayed activation and deactivation
All this ensures safe and trouble-free operation of the pumping station, even under demanding conditions.
The device is operated and configured using an intuitive resistive touchscreen, which displays all system parameters and functions. Each setting is saved in memory, so that after restarting, the pumping station automatically resumes operation according to the last configuration.
Additionally, the controller automatically records and stores the history of errors and events, which can be viewed on the touchscreen at any time, greatly facilitating system diagnostics and servicing.